

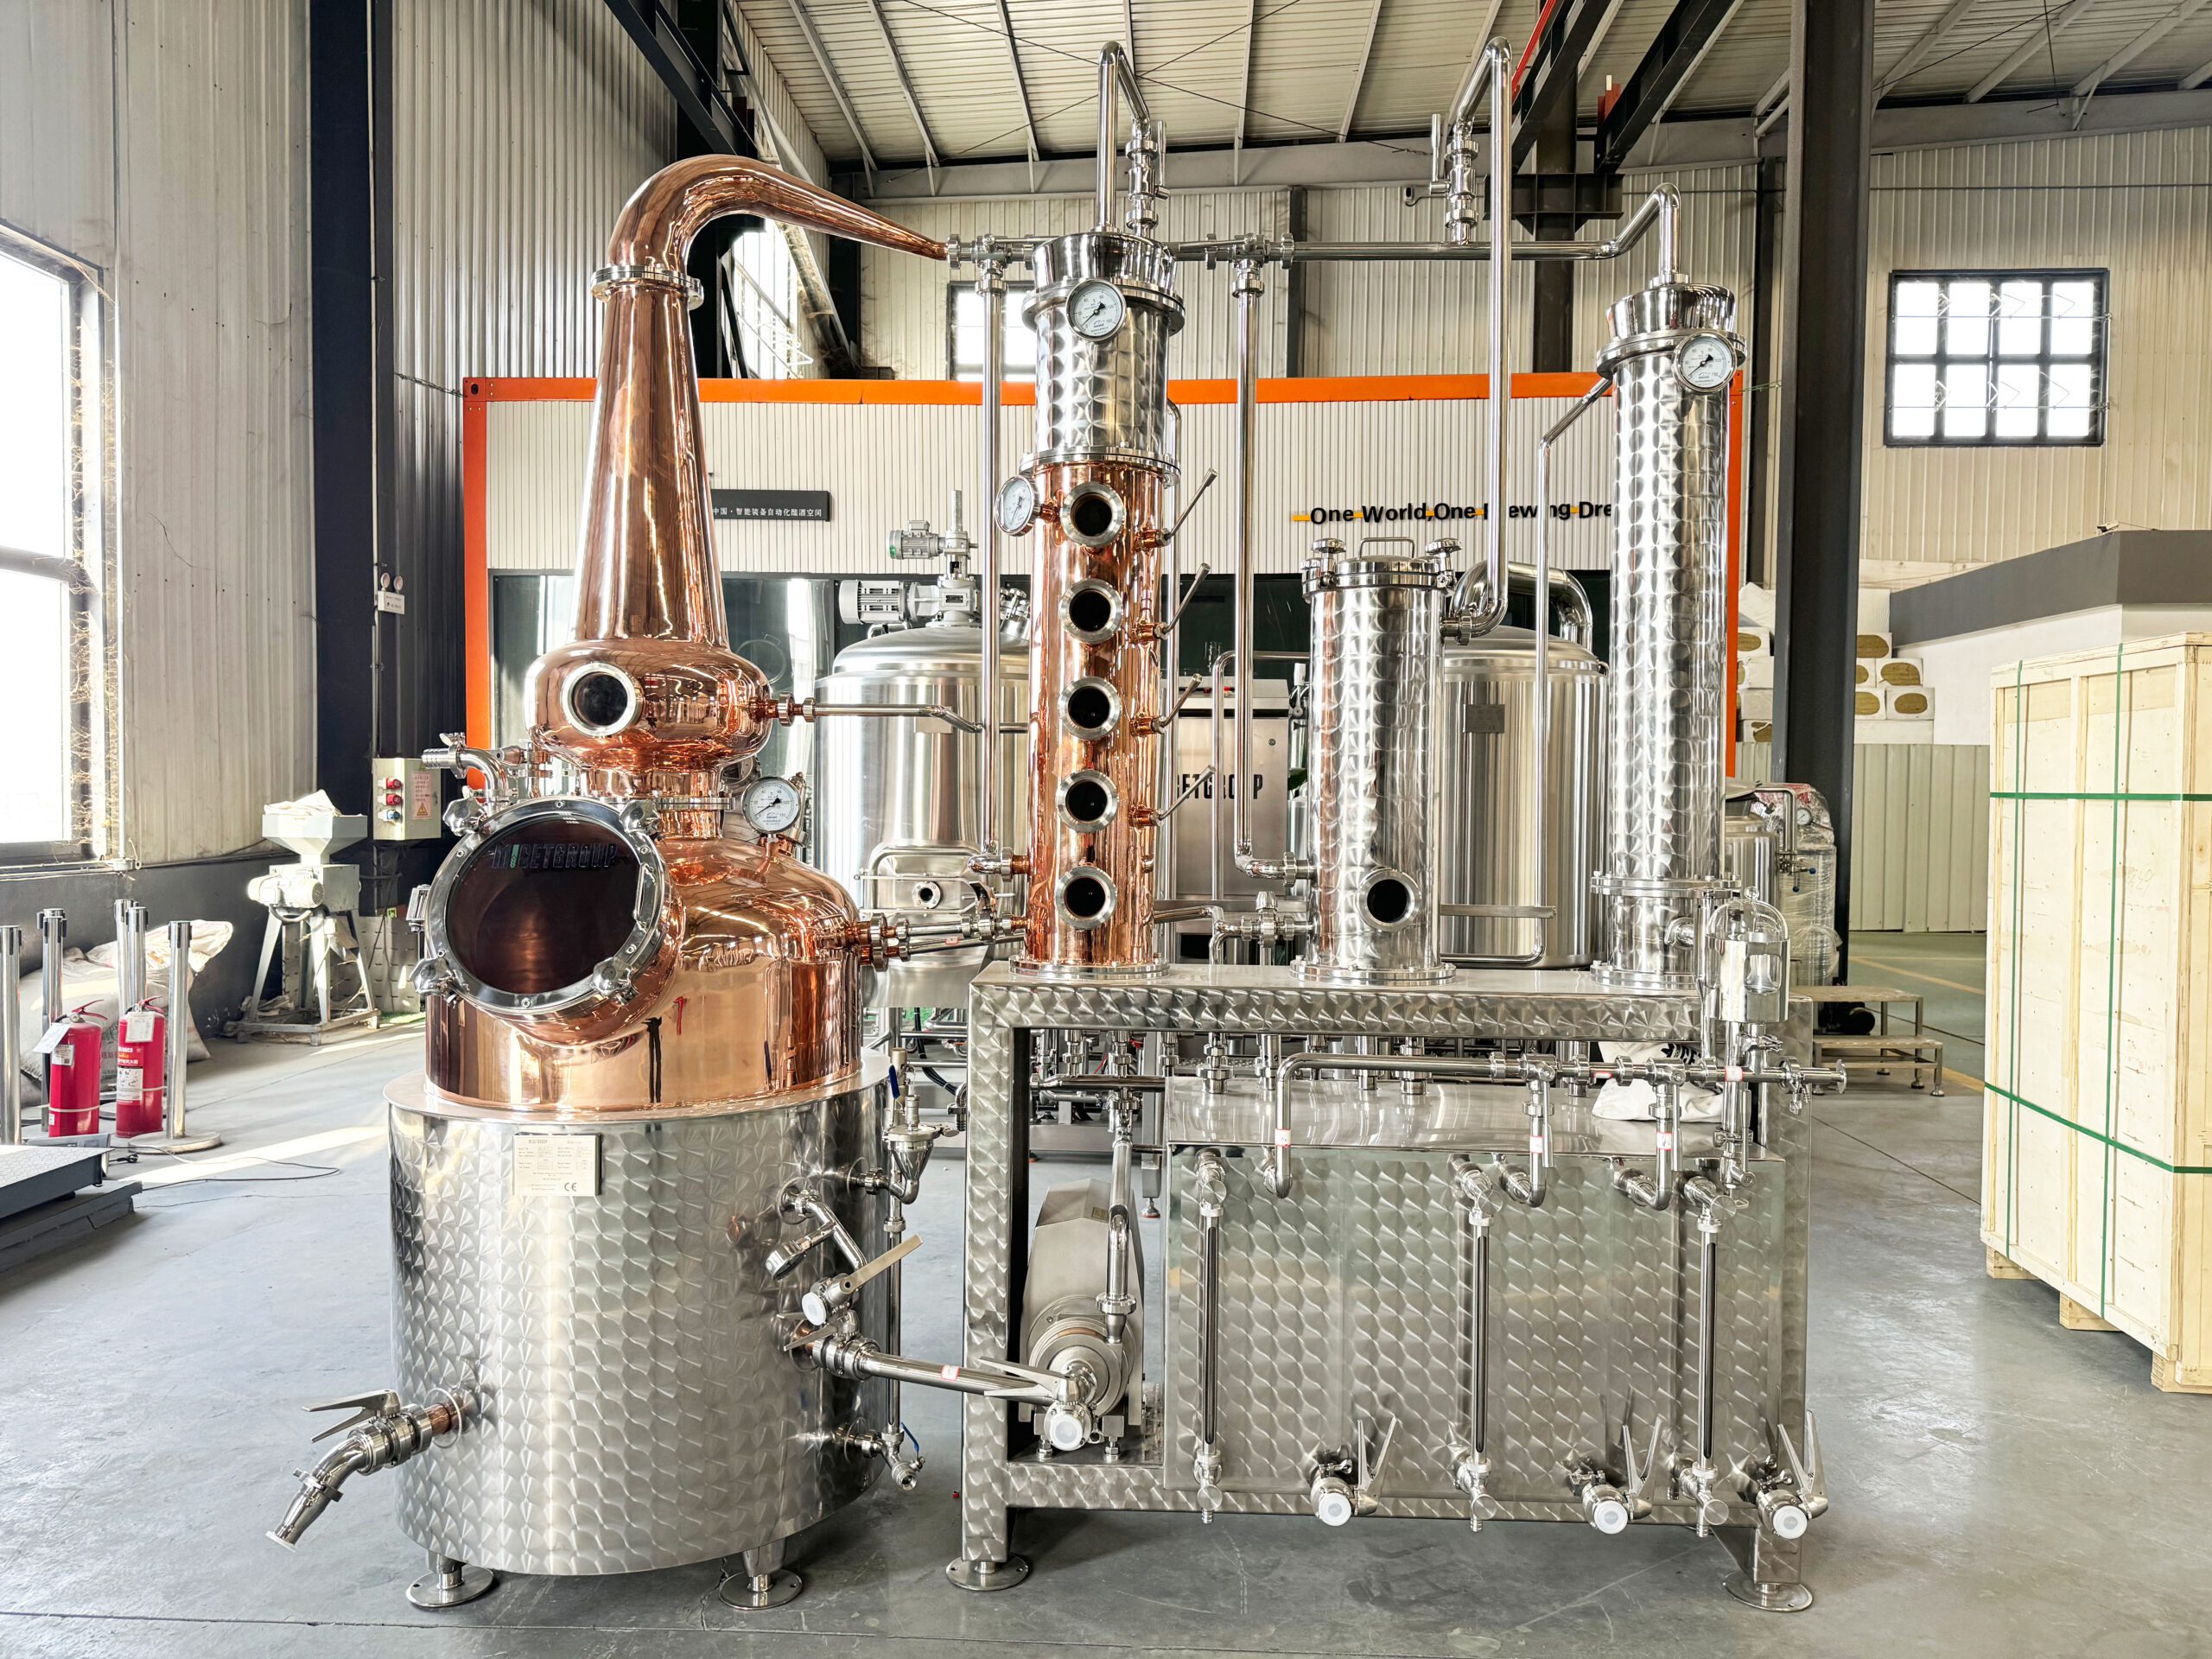
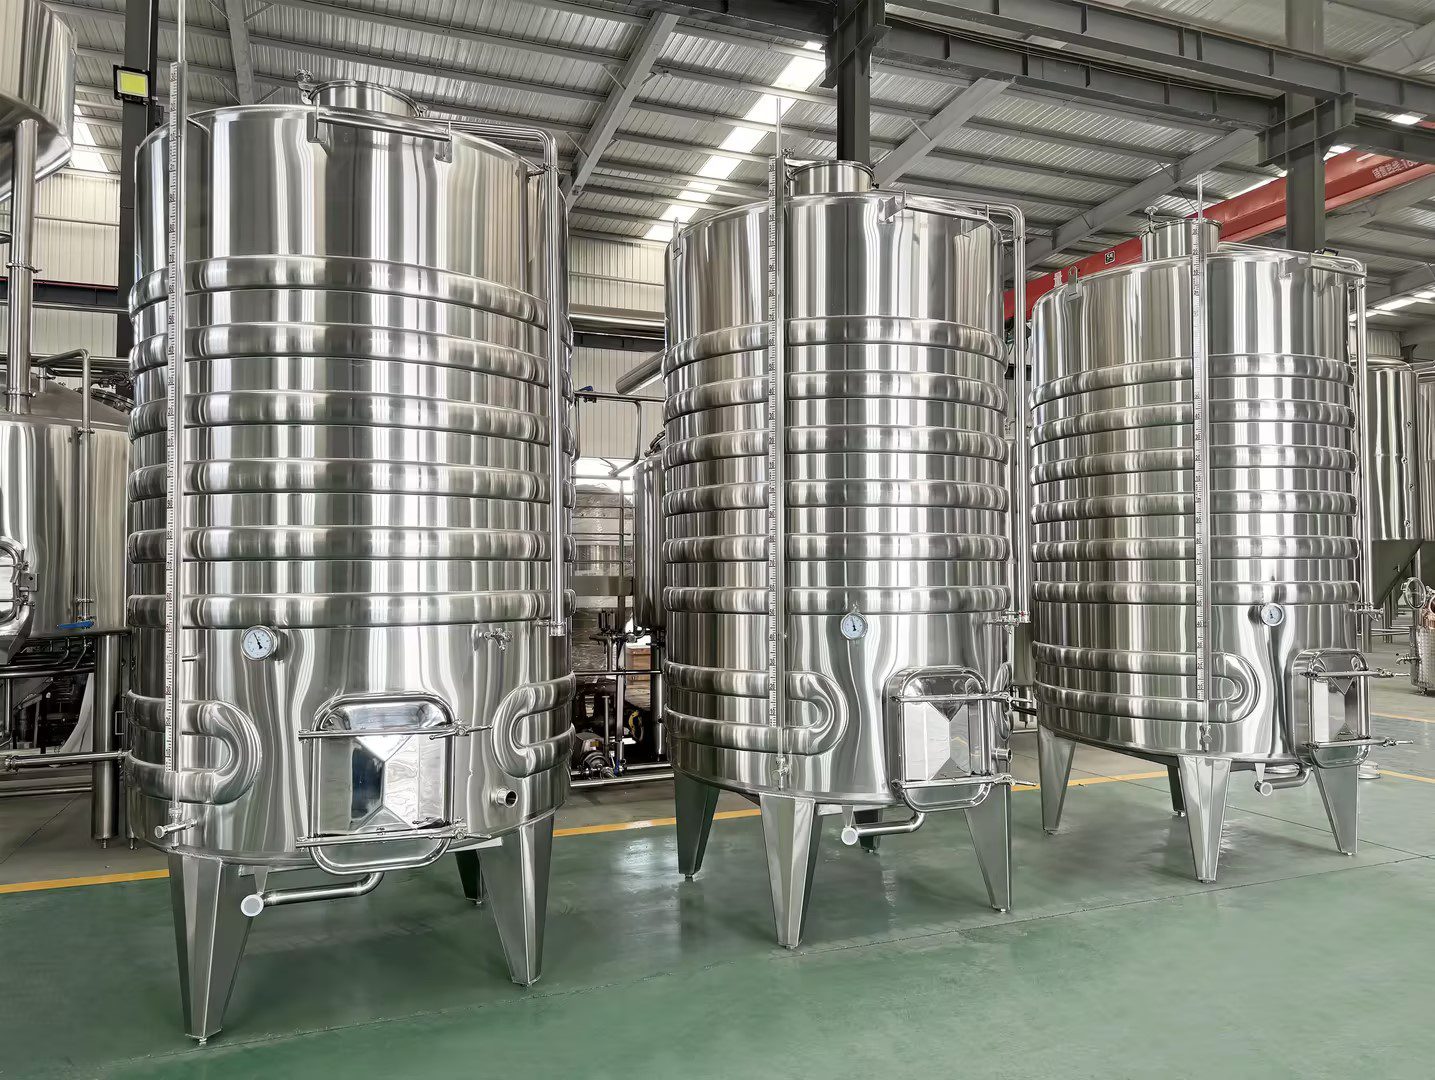
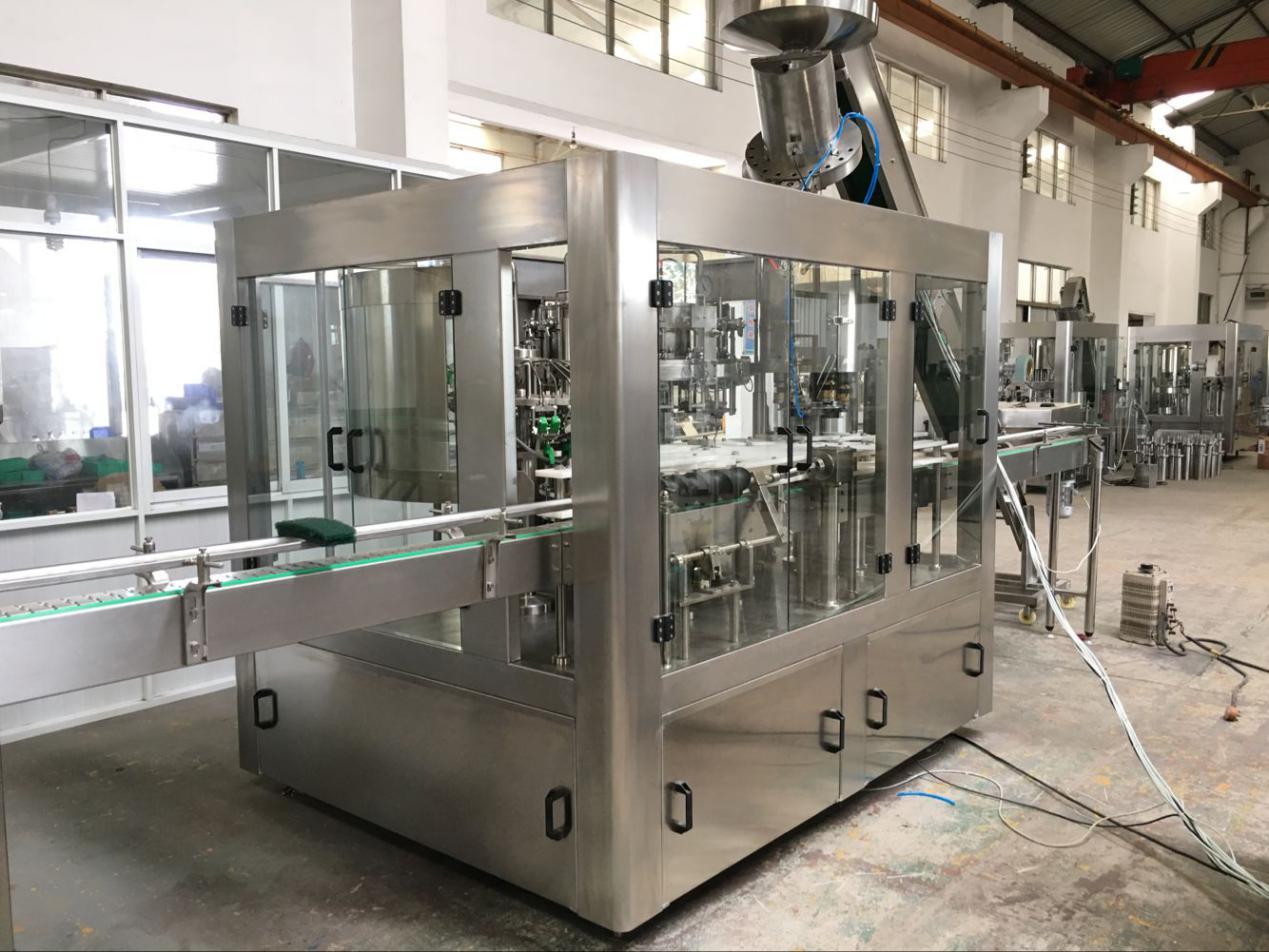
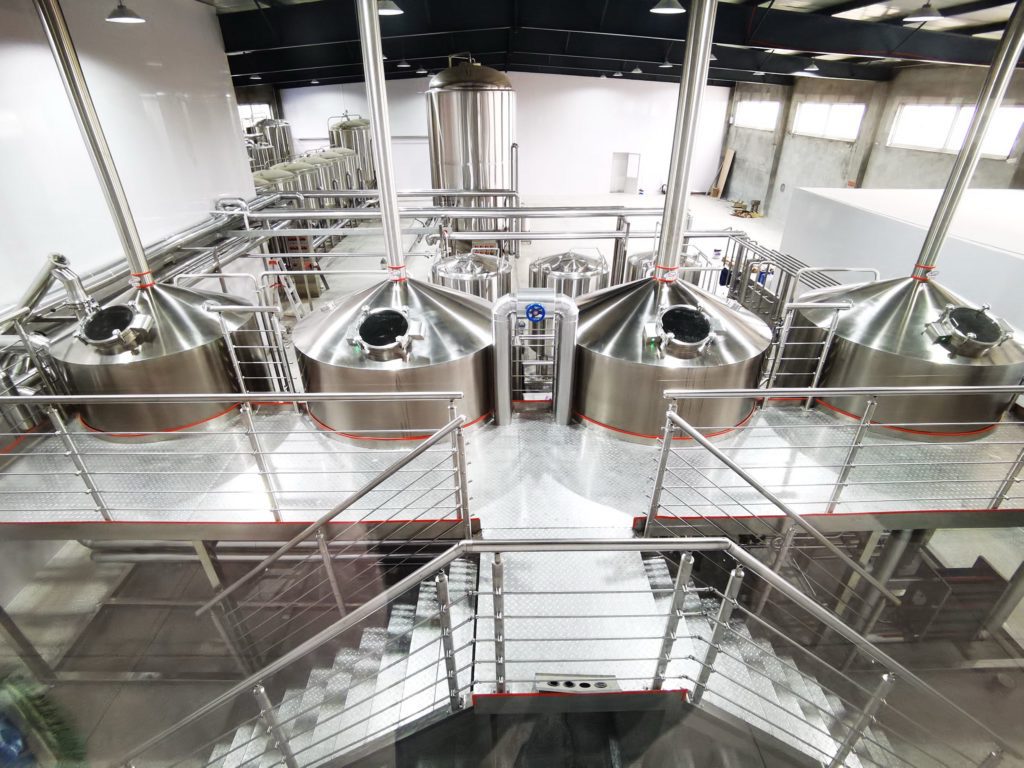
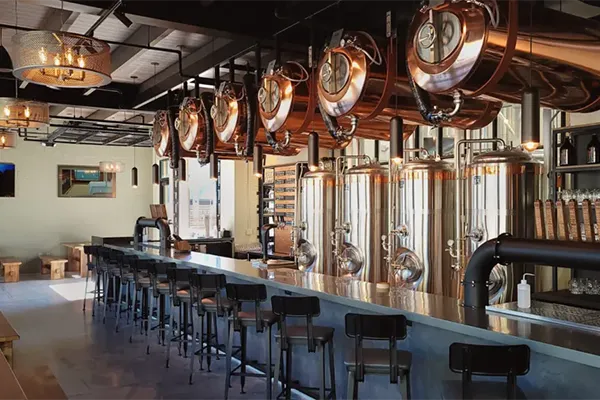
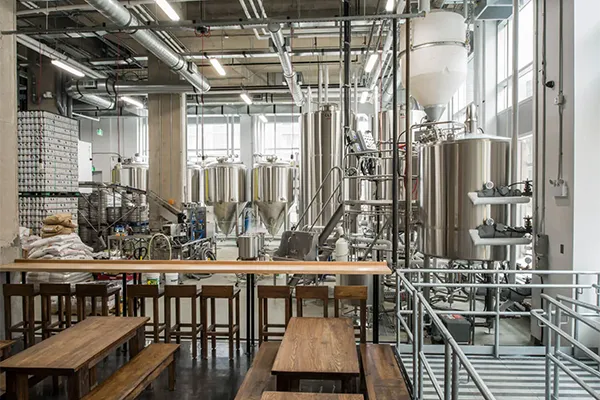
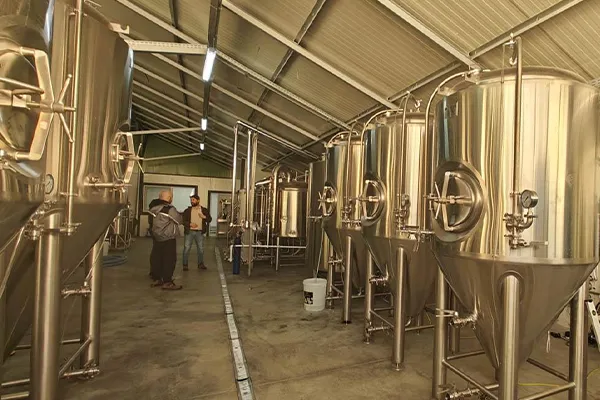
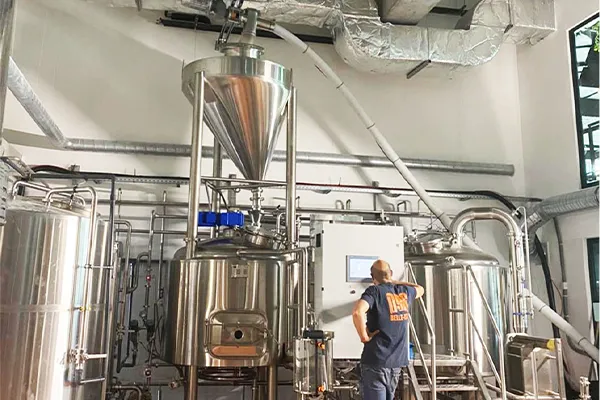
Distillery Machinery Suppliers: How to Choose the Right Distillery Equipment Manufacturer
Starting a distillery requires more than selecting a still. Many new beverage businesses face challenges such as unstable production, poor equipment compatibility, difficult maintenance, and unexpected expansion costs. Choosing reliable distillery machinery suppliers helps ensure efficient production, consistent spirits quality, and long-term business growth.
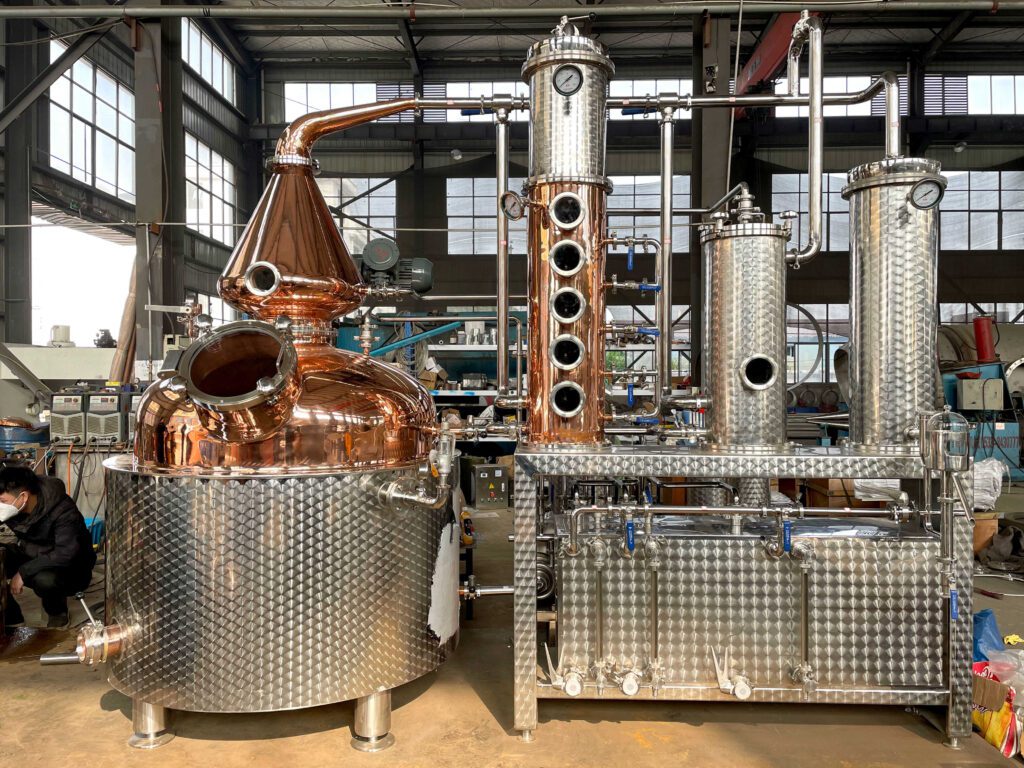
Distillery machinery suppliers provide equipment such as distillation systems, fermentation vessels, storage tanks, stills, and complete production solutions for spirit manufacturers. The right supplier should offer sanitary stainless steel equipment, customized engineering, installation support, and after-sales service based on your production capacity and product requirements.
What Do Distillery Machinery Suppliers Provide?
A professional distillery machinery supplier does more than sell individual machines. They help customers design complete production systems based on the type of spirits being produced, expected output, available space, and future expansion plans.
Modern distilleries may require:
| Equipment | Main Function |
|---|---|
| Fermentation tanks | Prepare fermented liquid before distillation |
| Distillation stills | Separate alcohol through controlled heating |
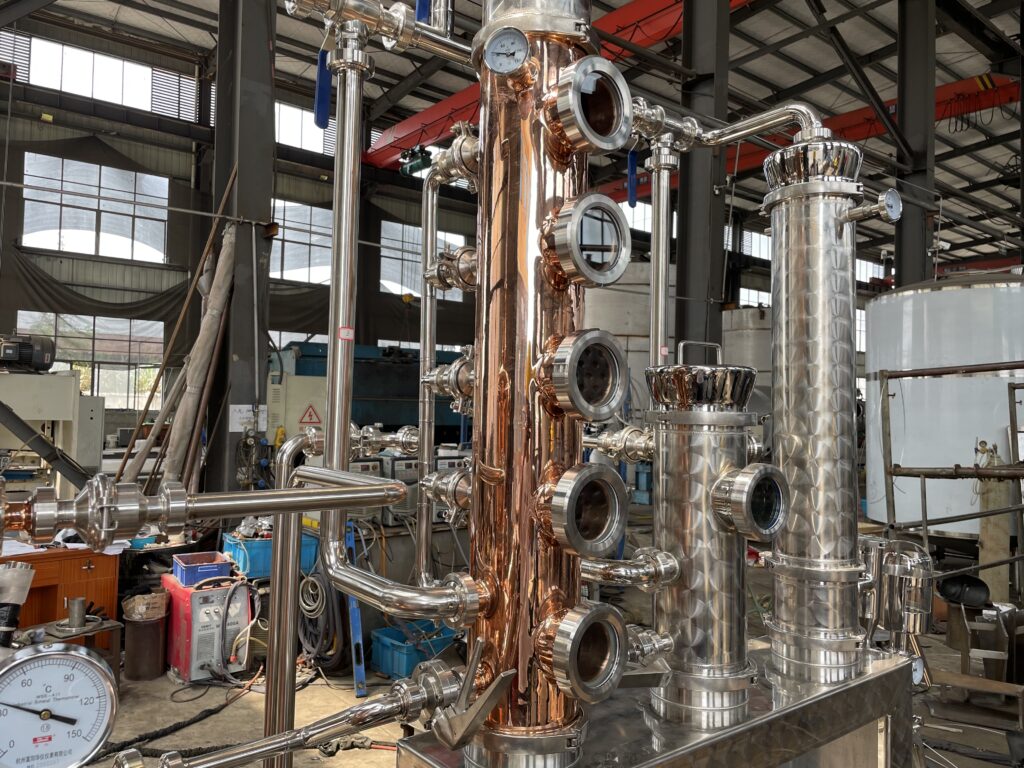
| Condensers | Convert vapor into liquid spirit |
| Storage tanks | Hold finished products |
| CIP systems | Support cleaning and sanitation |
| Filling equipment | Prepare products for packaging |
For beverage startups, wineries, craft spirit producers, and commercial distilleries, selecting the correct equipment supplier can significantly reduce project risks.
As a professional brewery and beverage equipment manufacturing plant, we provide customized stainless steel brewing systems, fermentation tanks, brewhouse systems, and turnkey beverage solutions for global B2B customers.
How Does Distillery Equipment Support the Distillation Process?
The distillation process depends on precise control of temperature, pressure, and material flow. High-quality machinery helps operators separate alcohol efficiently while maintaining product characteristics.
A complete distillery production line normally includes several connected stages:
- Raw material preparation
- Fermentation
- Distillation
- Cooling and condensation
- Storage and maturation
- Packaging
Each stage requires equipment designed for reliable operation.
For example, fermentation tanks must provide stable conditions for yeast activity, while distillation machinery must control vapor movement and condensation. Poor equipment design can affect flavor consistency and production efficiency.
What Types of Distillery Machinery Do Suppliers Offer?
Different spirits require different equipment configurations. A supplier should understand the relationship between product style, production volume, and machinery design.
Common distillery machinery includes:
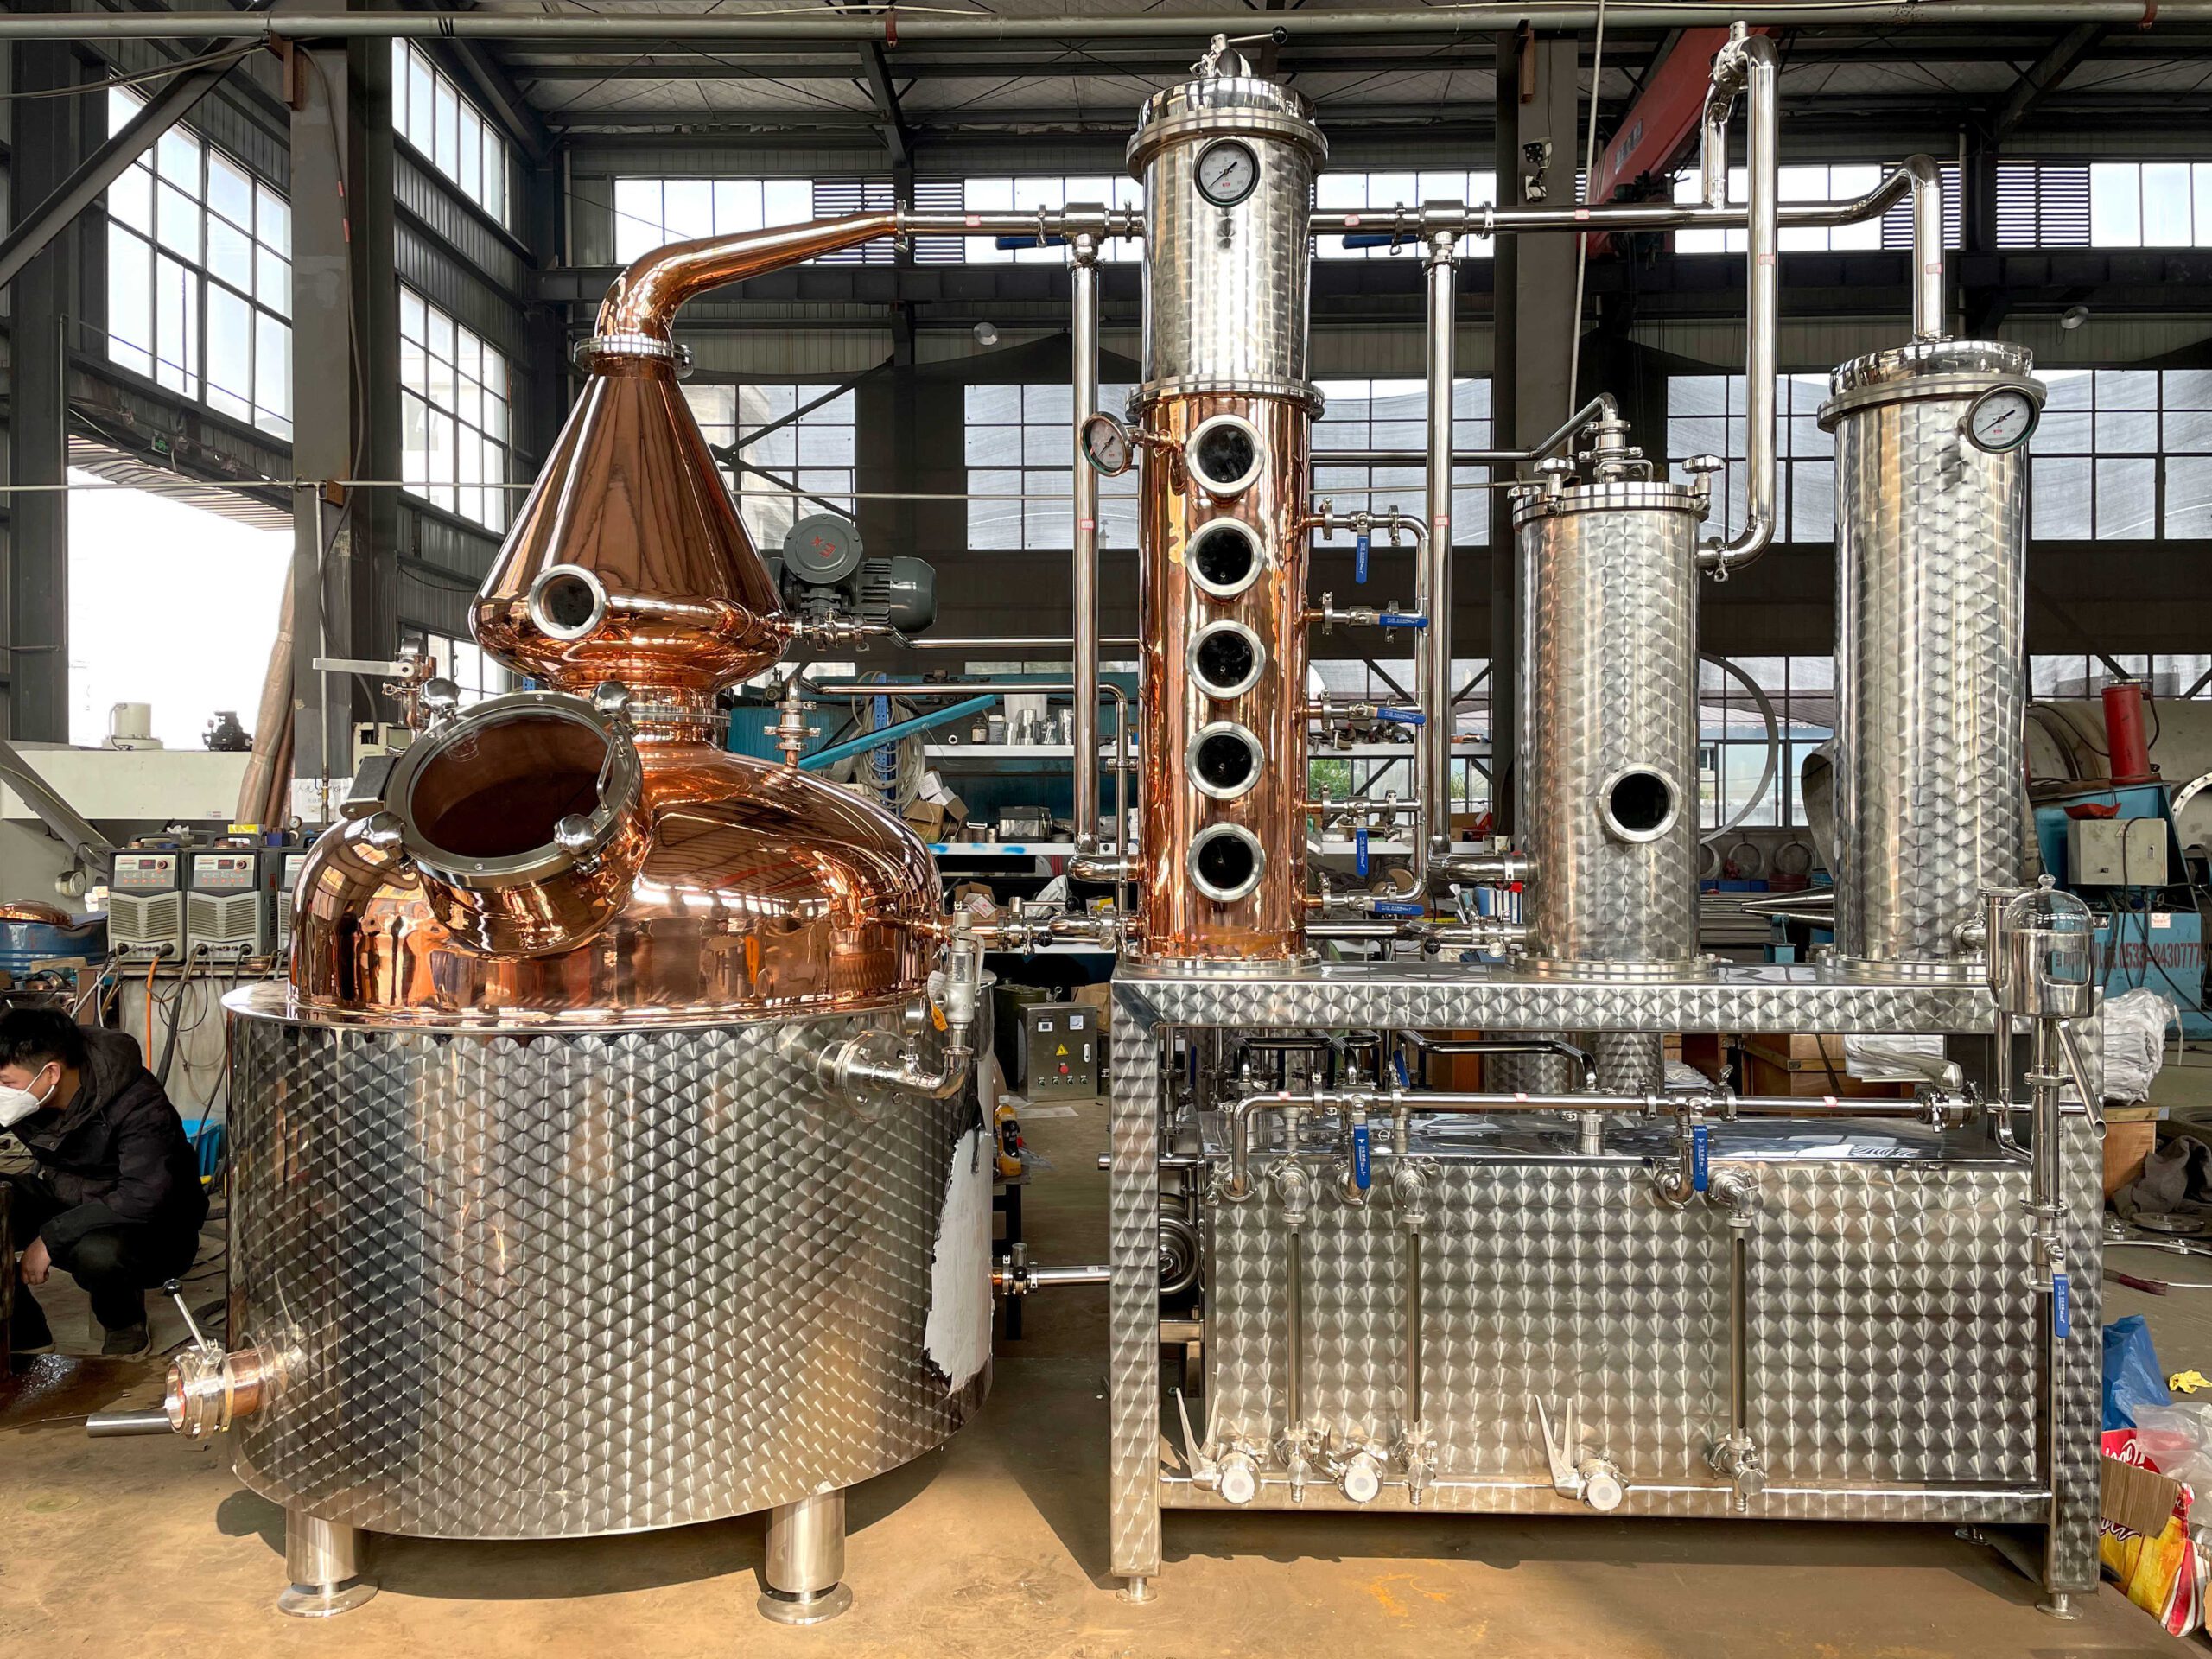
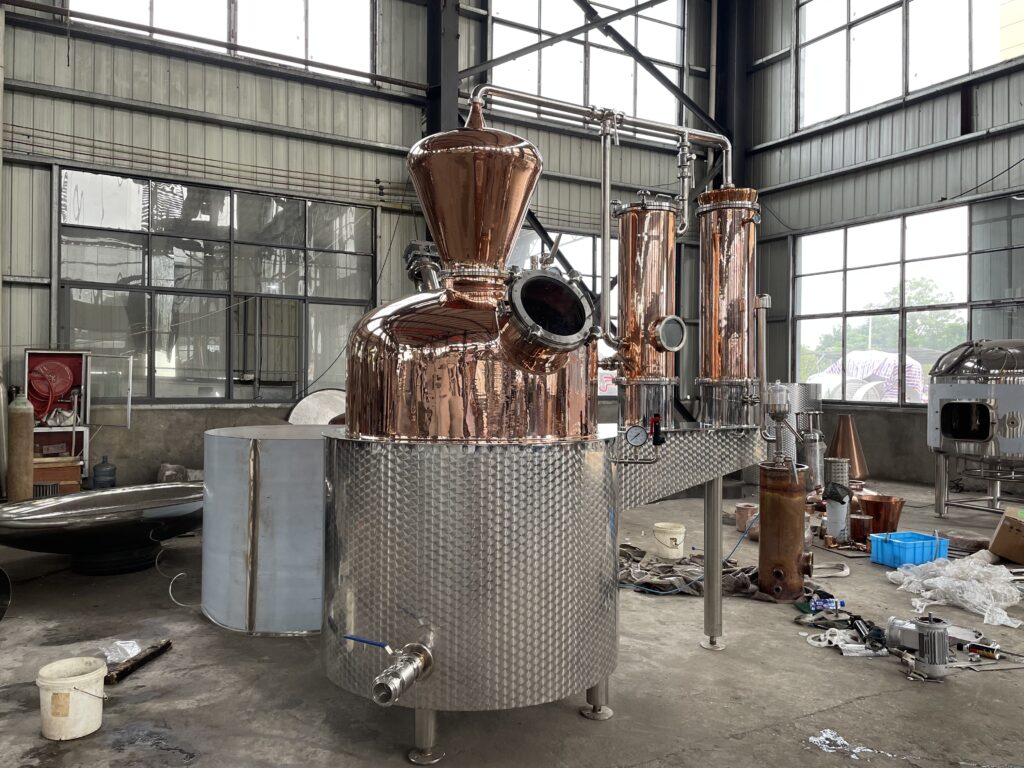
Pot Still Systems
Pot stills are commonly used for traditional spirits where flavor retention is important. They allow distillers to carefully control heating and separation.
Column Distillation Systems
Column systems are designed for continuous production and higher efficiency. They are often used by larger commercial distilleries.
Fermentation Equipment
Fermentation vessels prepare the alcohol base before distillation. These tanks require sanitary construction and reliable temperature management.
Storage and Aging Tanks
Storage tanks help manage production flow and maintain product quality before packaging.
The right combination depends on whether you operate a small craft distillery or a large-scale production facility.
Why Is Stainless Steel Important for Distillery Machinery?
Most professional distillery equipment uses stainless steel because it offers excellent durability, hygiene, and corrosion resistance.
Advantages include:
- Easy cleaning
- Long service life
- Food-grade safety
- Stable performance
- Reduced contamination risk
For beverage production, material quality directly affects product safety and consistency.
High-quality stainless steel tanks and distillation equipment provide smoother internal surfaces, making cleaning easier and improving overall sanitation.
A reliable supplier should consider not only equipment appearance but also welding quality, surface finishing, pressure standards, and long-term operation.
How Can You Choose the Right Distillery Machinery Supplier?
Choosing a supplier requires more than comparing equipment prices. A suitable partner should understand your business goals and provide complete technical support.
Important evaluation factors include:
| Factor | Why It Matters |
|---|---|
| Manufacturing experience | Ensures equipment reliability |
| Custom design capability | Matches your production needs |
| Material quality | Improves durability |
| Installation support | Reduces project delays |
| After-sales service | Supports long-term operation |
A professional supplier should ask questions such as:
- What type of spirits will you produce?
- What is your planned annual output?
- Do you need batch or continuous production?
- What production space is available?
- What level of automation do you require?
Good equipment planning starts before manufacturing begins.
What Equipment Is Needed for a Commercial Distillery?
A commercial distillery usually requires a complete production system rather than a single machine.
Typical equipment includes:
- Malt or raw material handling systems
- Fermentation vessels
- Distillation equipment
- Cooling systems
- Storage tanks
- Transfer pumps
- Control panels
- Packaging systems
The equipment configuration depends on production scale.
A startup distillery may begin with compact machinery, while an established company may require multiple fermentation tanks, larger stills, and automated production systems.
Professional distillery machinery suppliers help customers create scalable solutions that support future growth.
How Do Suppliers Customize Distillery Machinery for Different Projects?
Every distillery has different requirements. A rum producer, whisky producer, vodka manufacturer, and botanical spirit producer may need different equipment designs.
Customization may include:
- Tank volume
- Still design
- Heating method
- Automation level
- Pipeline layout
- Control system
- Production capacity
For example, a craft distillery focused on premium spirits may prioritize flexible batch production. A commercial producer may focus on efficiency and higher output.
A complete engineering approach ensures all equipment works together smoothly.
How Does Automation Improve Distillery Production?
Automation helps distilleries improve consistency and reduce manual operation.
Modern systems may include:
- Temperature monitoring
- Automatic valves
- Digital controls
- Process tracking
- Production data management
Automation supports repeatable production by reducing human error.
For growing beverage companies, automation can improve:
- Production efficiency
- Product consistency
- Labor management
- Quality control
However, automation should match the actual needs of the business. A supplier should recommend practical solutions rather than unnecessary complexity.
Why Should Distilleries Work With Turnkey Equipment Suppliers?
Building a distillery involves many technical decisions. Working with a turnkey supplier simplifies the process by connecting equipment design, manufacturing, installation, and service.
A turnkey solution may include:
- Production planning
- Equipment layout
- Manufacturing
- Transportation
- Installation guidance
- Technical training
This approach reduces coordination problems between different suppliers.
For international customers, reliable communication and technical support are especially important. A complete solution provider helps customers move from concept to production more efficiently.
What Should You Ask Before Buying Distillery Machinery?
Before purchasing equipment, buyers should prepare a detailed project plan.
Important questions include:
Production Questions
- What volume do you want to produce?
- What products will you manufacture?
- How much expansion do you expect?
Equipment Questions
- What materials are used?
- How is cleaning performed?
- What maintenance is required?
Supplier Questions
- Do you provide installation support?
- Can equipment be customized?
- Do you offer spare parts and technical assistance?
A detailed discussion helps prevent costly changes later.
How Can a Professional Equipment Manufacturer Support Your Distillery Project?
Selecting experienced distillery machinery suppliers gives businesses access to engineering knowledge, manufacturing capability, and long-term support.
Our company provides customized stainless steel beverage equipment solutions for:
- Distilleries
- Breweries
- Beverage startups
- Kombucha producers
- Wineries
- Engineering contractors
We focus on:
- Sanitary equipment design
- Stable production performance
- Customized capacity planning
- Efficient production layouts
- Reliable installation support
From fermentation tanks to complete distillation systems, professional equipment design helps beverage companies build reliable production operations.
Frequently Asked Questions
What equipment do distillery machinery suppliers provide?
Distillery machinery suppliers typically provide fermentation tanks, distillation systems, storage tanks, condensers, pumps, control systems, and packaging solutions.
How do I choose a reliable distillery equipment supplier?
Choose suppliers with manufacturing experience, customization capability, quality materials, installation support, and proven beverage industry experience.
Why is stainless steel used for distillery equipment?
Stainless steel provides corrosion resistance, easy cleaning, durability, and sanitary performance required for beverage production.
Can distillery machinery be customized?
Yes. Professional suppliers can customize tank sizes, production capacity, automation levels, and system layouts according to project requirements.
Do suppliers provide complete distillery solutions?
Many experienced suppliers provide turnkey solutions covering design, manufacturing, installation guidance, and technical support.
Key Points to Remember
- Distillery machinery suppliers provide essential equipment for spirit production, from fermentation to packaging.
- Choosing the right supplier is important for production efficiency, quality control, and future expansion.
- Stainless steel equipment supports sanitary operation and long-term durability.
- A complete distillery system should match your product type, production capacity, and business goals.
- Turnkey equipment suppliers can simplify project management and reduce production risks.
- Professional engineering support helps create a reliable distillery that can grow with your business.
Commercial Kombucha Brewing Equipment: Complete Guide to Kombucha Brewing Equipment for Commercial Production
Starting a commercial kombucha business requires more than a recipe and fermentation knowledge. Without the right kombucha brewing equipment, producers may struggle with inconsistent flavor, poor sanitation, limited production capacity, and difficult scaling. A customized stainless steel brewing system helps transform small-batch ideas into reliable commercial production.
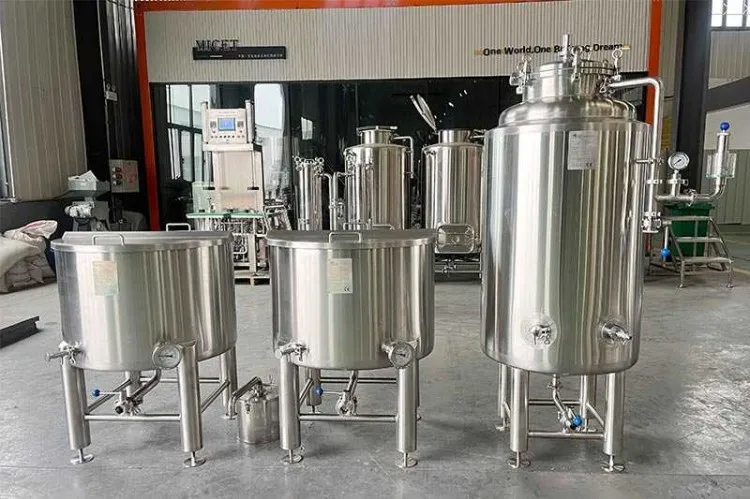
Commercial kombucha brewing equipment includes brewing kettles, fermentation tanks, stainless steel fermenters, carbonation systems, storage vessels, and packaging equipment designed for large-scale kombucha production. The right system helps kombucha producers control fermentation, maintain sanitation, improve consistency, and expand production efficiently.
What Equipment Is Needed for Commercial Kombucha Brewing?
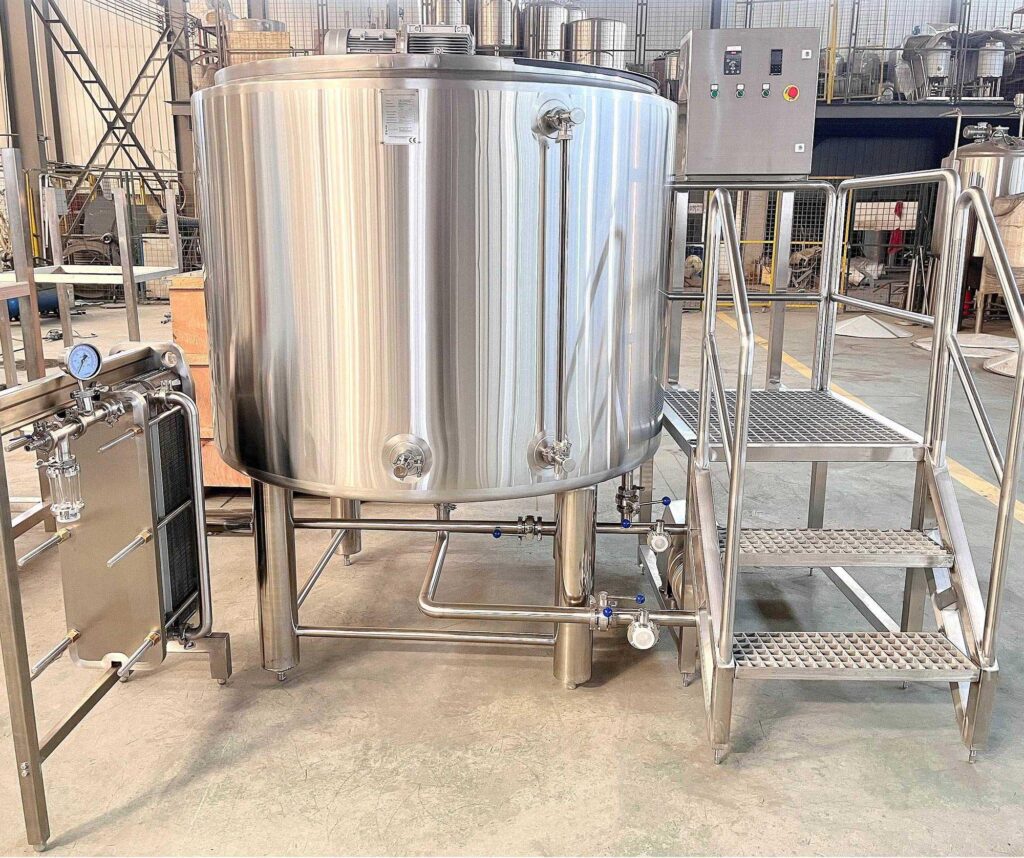
Commercial kombucha production requires specialized equipment that supports every stage of the brewing process. Unlike small home operations, a professional kombucha brewery needs equipment that can handle larger batch volumes while maintaining stable quality.
A complete kombucha brewing system usually includes:
| Equipment | Function |
|---|---|
| Brewing kettle | Prepares sweet tea base |
| Fermentation tanks | Supports primary fermentation |
| Stainless steel fermenter | Controls fermentation conditions |
| Brite tank | Carbonation and storage |
| CIP system | Cleaning and sanitation |
| Packaging equipment | Bottling or kegging |
For a growing kombucha brand, equipment selection directly affects production capacity, product consistency, and operating costs. A professional equipment supplier can help design a system based on expected sales volume, available space, and future expansion plans.
As a manufacturer of customized beverage equipment, we provide stainless steel brewing systems, fermentation tanks, and turnkey solutions for global B2B customers who need reliable commercial kombucha equipment.
How Does a Commercial Kombucha Brewing System Work?
A commercial kombucha brewing system follows a controlled production process that converts sweet tea into fermented kombucha.
The typical process includes:
- Preparing sweet tea
- Cooling the liquid
- Adding SCOBY culture
- Primary fermentation
- Flavor adjustment
- Secondary fermentation
- Carbonation
- Packaging
During fermentation, the symbiotic culture of bacteria and yeast transforms sugar into organic acids, flavors, and natural carbonation.
A professional system gives producers better control over:
- Fermentation time
- Temperature
- Oxygen exposure
- Sanitation
- Batch consistency
For commercial kombucha brewing, repeatability is critical. Customers expect the same taste and quality from every bottle or keg.
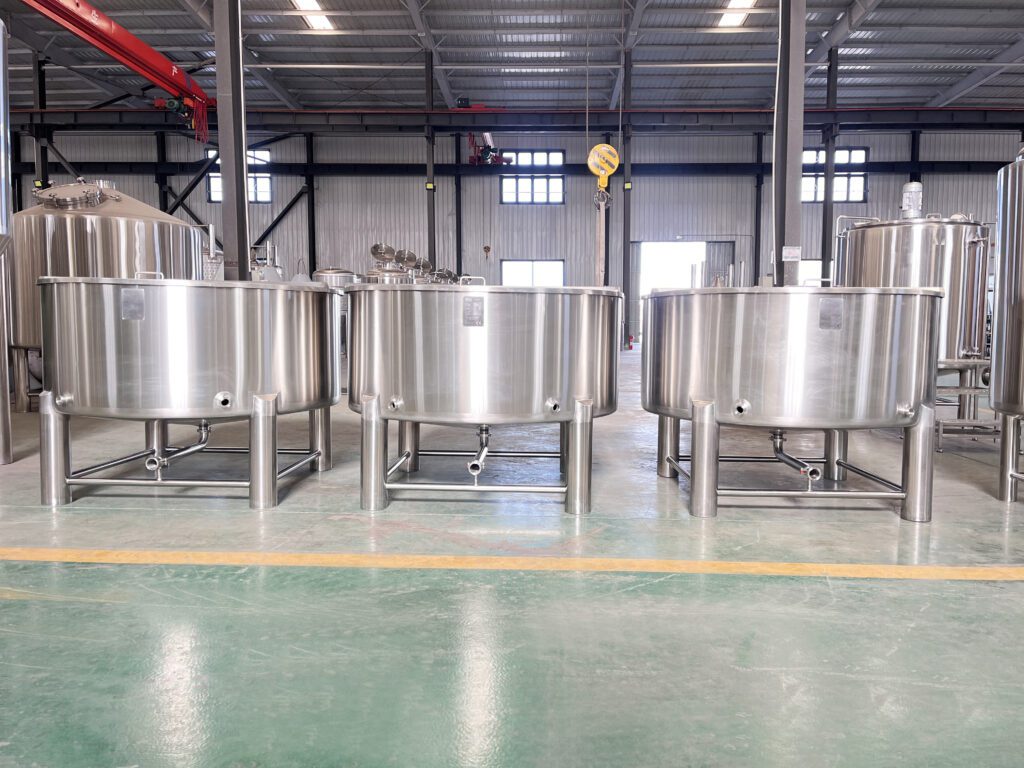
Why Is Stainless Steel Important for Kombucha Brewing Equipment?
Material selection is one of the most important decisions when choosing kombucha brewing equipment.
High-quality stainless steel is widely used because it provides:
- Excellent corrosion resistance
- Easy cleaning
- Long service life
- Food-grade safety
- Better sanitation control
Compared with steel or plastic alternatives, stainless steel tanks provide a more stable environment for fermentation.
A stainless steel fermenter allows producers to maintain consistent conditions while reducing contamination risks. Smooth internal surfaces make cleaning easier and support professional sanitation practices.
For commercial kombucha producers, stainless steel equipment is not only about durability. It supports quality kombucha brewing and long-term business growth.
What Are the Main Types of Kombucha Brewing Equipment for Commercial Production?
Different businesses require different equipment configurations. A small kombucha startup may need a compact system, while a large kombucha brewery may require multiple fermentation vessels and automated controls.
Common equipment includes:
Brewing Kettle
The kettle prepares the tea base before fermentation. Producers typically use black or green tea combined with sugar to create sweet tea.
A properly designed kettle improves heating efficiency and simplifies cleaning.
Fermentation Tanks
Fermentation tanks are the heart of kombucha production. They provide controlled space where SCOBY and microorganisms develop flavor.
Modern fermentation tanks may include:
- Cooling jacket
- Temperature monitoring
- Sanitary valves
- Pressure control
Brite Tank
A brite tank supports carbonation, clarification, and storage before packaging.
For kombucha on tap products, brite tanks help maintain consistent carbonation levels.
How Do Fermentation Tanks Improve Commercial Kombucha Production?
Fermentation is the most sensitive stage of kombucha production. Small changes in temperature, time, or sanitation can affect flavor and quality.
Commercial fermentation tanks allow producers to control fermentation conditions more accurately.
Important features include:
- Temperature control
- Insulated tank design
- Glycol cooling systems
- Easy cleaning structure
- Pressure-rated construction
A stainless steel fermenter helps maintain stable fermentation temperature throughout the fermentation cycle.
For larger operations, multiple fermentation tanks allow different flavors or batches to ferment at the same time.
This flexibility helps kombucha brands increase production capacity without sacrificing consistency.
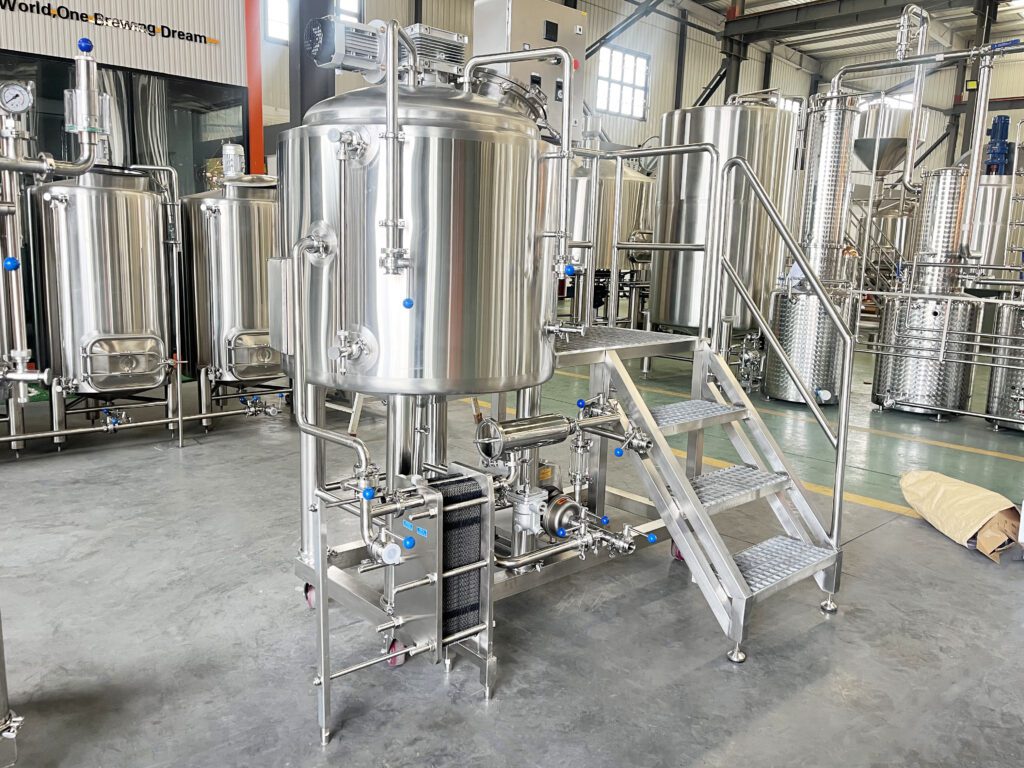
What Is the Difference Between Home Brewing and Commercial Kombucha Brewing?
Home brewing and commercial kombucha production share the same basic principles, but the equipment requirements are very different.
| Feature | Home Brewing | Commercial Production |
|---|---|---|
| Batch Size | Small | Large |
| Equipment | Simple containers | Stainless steel systems |
| Control | Manual | Automated monitoring |
| Cleaning | Basic | CIP sanitation |
| Packaging | Small bottles | Professional filling systems |
A home brewer may successfully produce kombucha in small quantities. However, commercial production requires reliable equipment that can operate batch after batch.
A commercial kombucha brewery needs solutions designed for:
- Higher production capacity
- Better process control
- Consistent flavor
- Reduced contamination risk
How Does Temperature Control Affect Kombucha Fermentation?
Temperature control plays an important role in kombucha fermentation.
The fermentation environment influences:
- Acidity development
- Flavor profile
- Carbonation
- Fermentation speed
A professional fermentation tank with a cooling jacket helps maintain stable fermentation temperature.
Many commercial systems use glycol cooling because it provides accurate temperature management.
Without proper control, fermentation may become inconsistent. This creates challenges for brands trying to scale production.
For this reason, temperature control is one of the most important features when selecting kombucha brewing equipment for commercial production.
What Sanitation Features Should Commercial Kombucha Equipment Have?
Sanitation is essential because kombucha contains active bacteria and yeast. While these microorganisms create the desired flavor, unwanted contamination can damage product quality.
Professional kombucha equipment should include:
- Smooth stainless steel surfaces
- Sanitary fittings
- CIP cleaning capability
- Easy-access valves
- Proper drainage
CIP systems allow operators to clean tanks and pipelines efficiently without manual disassembly.
A reliable sanitation system helps prevent contamination and protects every batch.
For commercial kombucha producers, cleaning and sanitizing is not just maintenance. It is part of product quality control.
How Can a Kombucha Brewery Scale Production Efficiently?
Scaling a kombucha business requires careful equipment planning.
Many producers start with a small system and later expand by adding:
- Larger fermentation tanks
- Additional storage tanks
- Automated controls
- Packaging equipment
- More production space
A good kombucha brewing system should support future growth.
When designing equipment, we consider:
- Production capacity
- Tank size
- Available space
- Product types
- Packaging methods
A kombucha brand selling bottled products may need different equipment compared with a company producing kombucha on tap.
How to Choose the Right Commercial Kombucha Equipment Supplier?
Selecting the right equipment supplier is an important step for any kombucha business.
A professional supplier should understand:
- Fermentation requirements
- Beverage production workflows
- Stainless steel fabrication
- Sanitary design
- Installation support
As an experienced beverage equipment manufacturer, we provide customized solutions for:
- Kombucha producers
- Breweries
- Beverage startups
- Craft beverage companies
- Engineering contractors
Our commercial kombucha equipment can include fermentation vessels, brewing systems, storage tanks, CIP solutions, and complete production lines.
The right equipment partner helps businesses produce consistent kombucha while reducing project risks.
Frequently Asked Questions
What equipment is needed for commercial kombucha production?
Commercial kombucha production typically requires brewing kettles, fermentation tanks, stainless steel fermenters, carbonation equipment, storage tanks, CIP systems, and packaging equipment.
Can stainless steel tanks be used for kombucha fermentation?
Yes. Stainless steel tanks are widely used for kombucha fermentation because they are durable, sanitary, easy to clean, and suitable for commercial production.
How large should a commercial kombucha fermentation tank be?
Tank size depends on production goals, batch volume, fermentation time, and future expansion plans. A supplier can help calculate the correct capacity.
Does kombucha require temperature control during fermentation?
Yes. Temperature control helps maintain consistent fermentation performance and improves product quality.
What is the difference between a kombucha fermenter and a regular beverage tank?
A kombucha fermenter is designed specifically for fermentation conditions, while general beverage tanks may only provide storage functions.
Key Points to Remember
- Commercial kombucha brewing requires specialized equipment beyond home brewing tools.
- Stainless steel fermentation tanks provide durability, sanitation, and reliable production.
- Temperature control and CIP systems are essential for consistent kombucha quality.
- A complete kombucha brewing system may include kettles, fermenters, brite tanks, and packaging equipment.
- Choosing the right equipment supplier helps reduce project risk and support business expansion.
- Customized commercial kombucha equipment allows brands to scale production while maintaining product consistency.
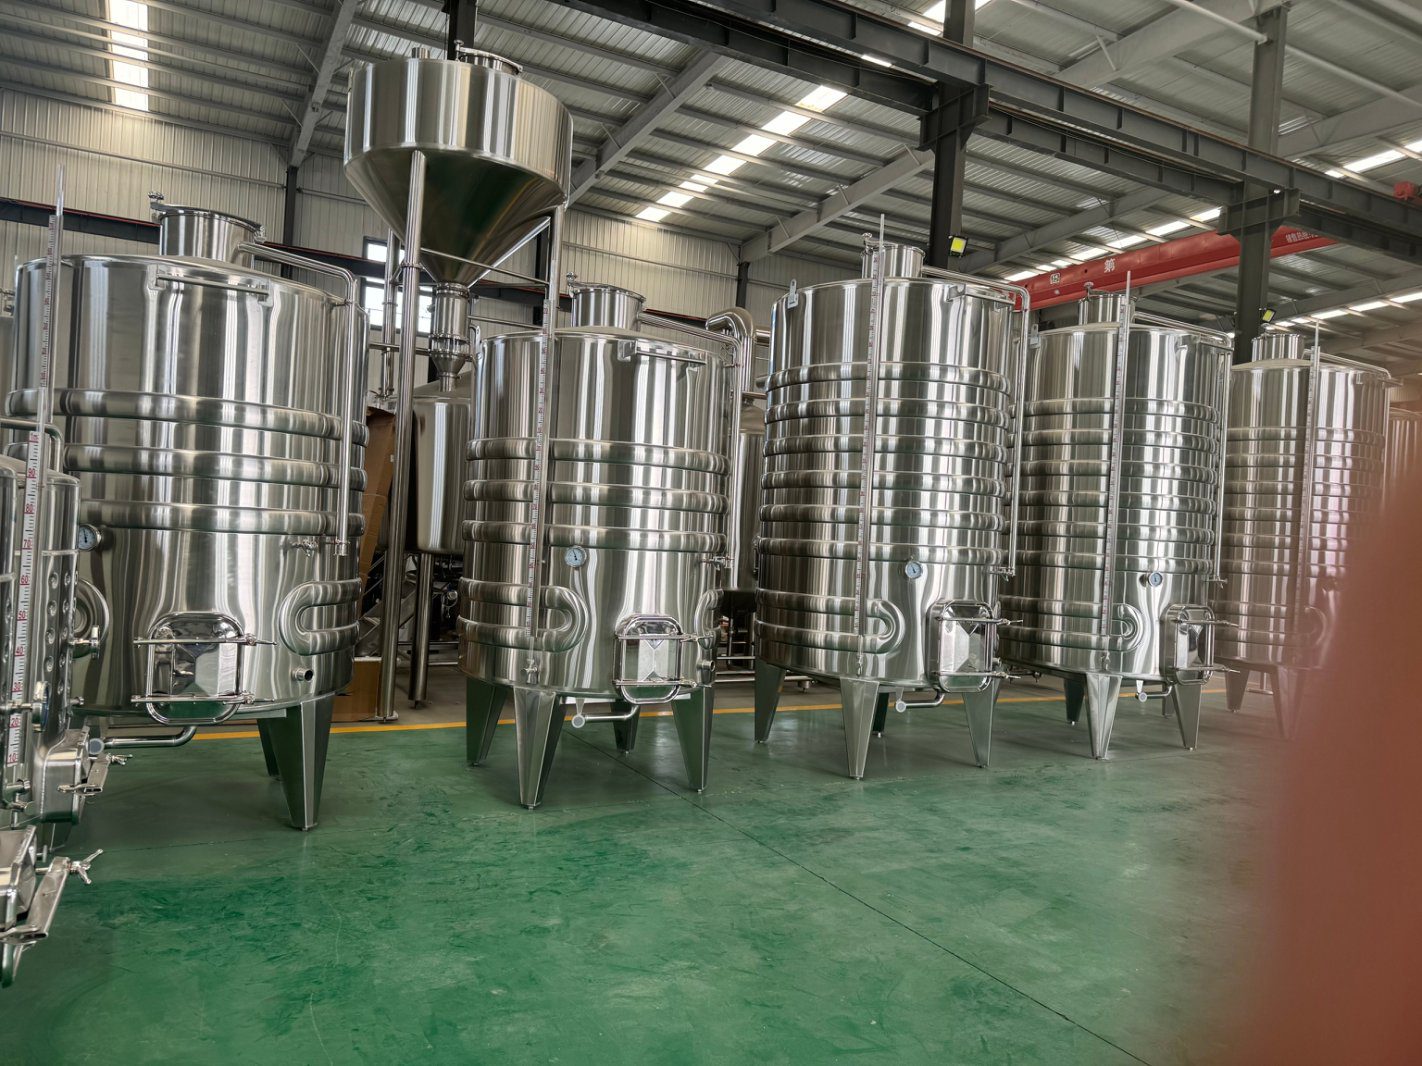
Used Stainless Steel Fermentation Tanks: What to Know Before Buying Used Fermenters
Buying used fermentation equipment may look like an affordable way to expand production, but the wrong tank can create hidden costs through repairs, poor sanitation, and limited compatibility. Before purchasing used fermenters, breweries need to check material quality, pressure rating, cooling systems, and production requirements.
Used stainless steel fermentation tanks are previously operated vessels designed for beer, wine, and beverage fermentation. Before buying used equipment, check the tank material, capacity, jacket condition, pressure rating, valves, fittings, and maintenance history. For many breweries, a new customized fermentation tank can provide better long-term reliability and production efficiency.
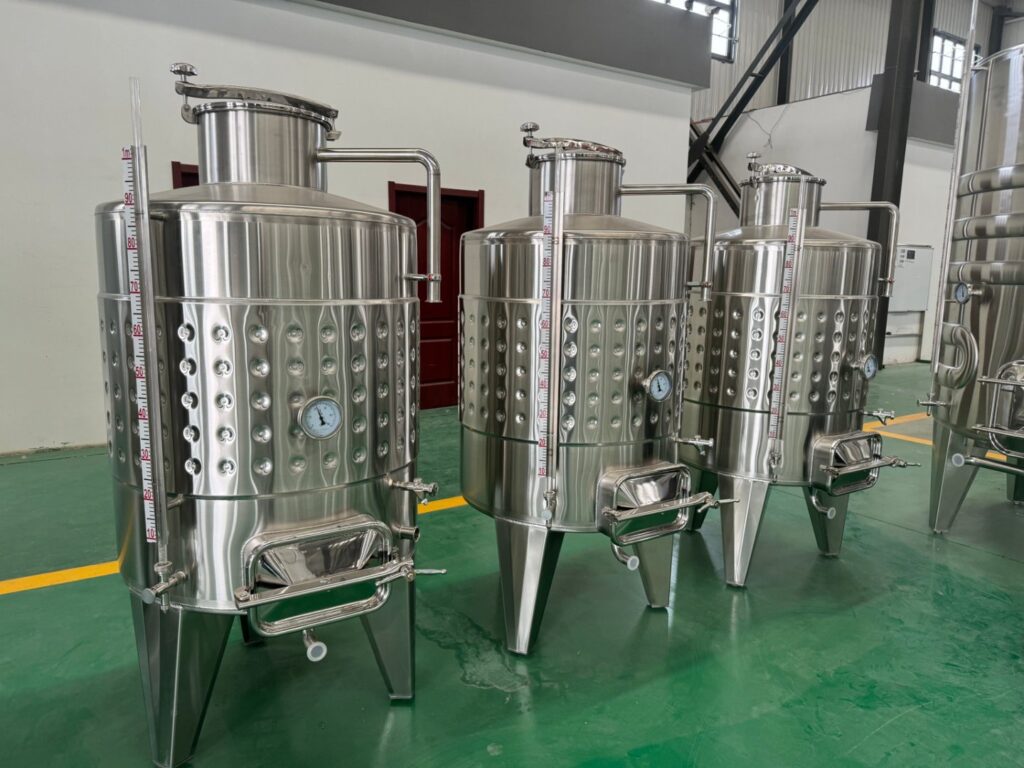
What Are Used Stainless Steel Fermentation Tanks?
Used stainless steel fermentation tanks are vessels that have previously been installed and operated in a brewery or beverage production facility. They are commonly sold when breweries upgrade their production lines, change capacity plans, or replace older equipment.
A fermentation tank, also called a fermenter or fermentor, is designed to hold liquid during the fermentation process. In beer production, yeast converts sugars into alcohol and carbon dioxide inside the tank. Similar tanks may also be used for wine, kombucha, and other beverage applications.
Most professional fermentation tanks are made from stainless steel because this material provides durability, corrosion resistance, and easy cleaning. Common designs include:
| Tank Feature | Purpose |
|---|---|
| Stainless steel body | Long service life and sanitary operation |
| Cooling jacket | Controls fermentation temperature |
| Cone bottom | Helps yeast collection |
| Pressure system | Supports controlled fermentation |
| Valves and fittings | Enables transfer and cleaning |
When searching for tanks for sale, buyers should look beyond appearance. A tank that looks clean externally may still require internal inspection, pressure testing, or replacement parts.
Why Do Breweries Buy Used Fermentation Tanks?
Many breweries choose used fermenters because they can reduce initial investment. For a startup brewery or expanding craft operation, used equipment may provide additional production capacity without the cost of purchasing every component new.
Common reasons businesses consider used fermentation tanks include:
- Increasing storage capacity quickly
- Adding extra fermentation space
- Supporting seasonal beer demand
- Testing a new production line
- Reducing startup costs
For example, a brewery may already have a brewhouse producing enough wort but lack enough fermentation capacity. Adding a used tank can solve that bottleneck faster than replacing the entire system.
However, used equipment is not always the most economical choice. Older tanks may require modifications, shipping, cleaning, pressure testing, or new controls. These costs should be included before making a purchase decision.
What Should You Check Before Buying Used Stainless Steel Fermentation Tanks?
A careful inspection is essential before purchasing used stainless steel fermentation tanks.
The most important factors include:
Material Quality
Check whether the tank is made from suitable stainless steel, such as 304 stainless steel. The internal surface should be smooth, clean, and free from corrosion or deep scratches.
Tank History
Ask:
- When was the tank installed?
- What product was fermented?
- How often was it cleaned?
- Has it been modified?
A tank manufactured in 2020 may have a very different condition from one installed many years earlier.
Pressure Rating
Fermentation tanks often operate under pressure. Confirm the pressure rating before connecting the tank to your brewery system.
A vessel rated for 15 psi, for example, may not be suitable for every production requirement.
Cooling System
Inspect the cooling jacket carefully. The jacket must work correctly with your glycol system to maintain stable fermentation temperatures.
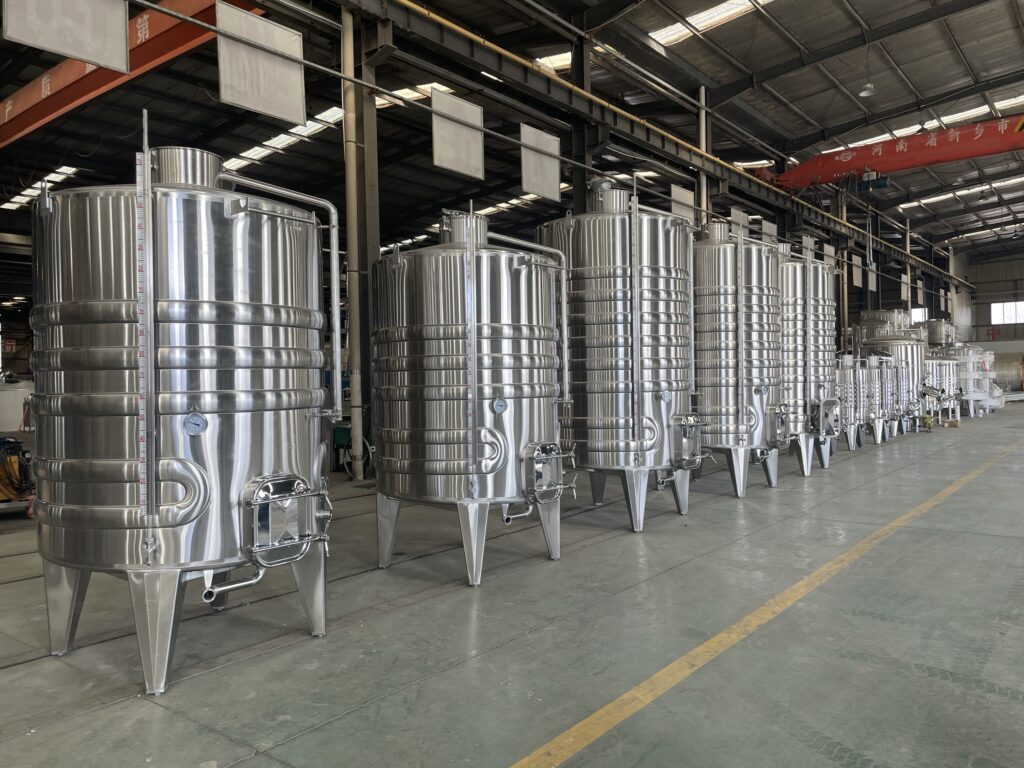
How Does a Fermentation Tank Work in a Brewery?
A fermentation tank receives cooled wort from the brewhouse after the brewing process. Yeast is added, and fermentation begins.
During fermentation:
- Yeast consumes sugars
- Alcohol and carbon dioxide are produced
- Temperature is controlled through the jacket
- Beer matures before transfer or packaging
A modern beer fermenter usually includes:
- Cooling jacket
- Pressure gauge
- Sampling valve
- Spray cleaning system
- Manway or manhole
- Product inlet and outlet
The cone design at the bottom helps collect yeast and sediment. This improves harvesting efficiency and makes cleaning easier.
For a brewery producing different beer styles, tank design affects flexibility. A well-designed fermenter supports consistent flavor and reliable production.
What Tank Sizes Are Available for Used Fermenters?
Used fermentation tanks come in many sizes depending on the previous production facility.
Common capacity ranges include:
| Capacity | Typical Application |
|---|---|
| Small litre tanks | Pilot brewing and small batches |
| 5–15 bbl tanks | Small craft breweries |
| 20–50 bbl tanks | Growing breweries |
| Larger tanks | Commercial production |
The correct tank size depends on your brewhouse output, fermentation time, and production schedule.
For example, purchasing an 800 gallon tank may sound attractive, but the brewery must confirm whether the volume matches existing brewhouses, pumps, piping, and cooling systems.
A tank that is too large may reduce flexibility. A tank that is too small may not solve production limitations.
Are Used Fermenters Better Than New Fermentation Tanks?
The answer depends on the project.
Used fermenters can provide:
Lower Purchase Cost
A used tank may be more affordable than new equipment.
Faster Availability
Some used tanks are already available from equipment inventory.
Short-Term Expansion
They can help breweries increase capacity quickly.
However, new fermentation tanks provide advantages:
- Customized dimensions
- New cooling jacket design
- Updated controls
- Exact capacity matching
- Full manufacturer support
As a professional brewery equipment manufacturer, we often recommend comparing the total project value rather than only the purchase price.
A lower-cost tank may require additional work, while a new customized fermentation tank can provide predictable performance for many years.
What Features Should a Quality Fermentation Tank Have?
A reliable fermentation tank should be designed around sanitation, temperature control, and efficient operation.
Important features include:
Cooling Jacket
The jacket allows glycol circulation to control fermentation temperature.
Some tanks use a dual glycol jacket system for improved cooling performance.
Insulation
A properly insulated tank helps maintain stable temperatures and reduces energy consumption.
Valves and Fittings
High-quality butterfly valves, sanitary fittings, and reliable connections make operation easier.
Cleaning System
A spray system and accessible manway help operators clean the tank effectively.
Pressure Control
A pressure system allows controlled fermentation and carbonation management.
These details separate professional brewing equipment from basic storage vessels.

How Can Used Fermentation Tanks Be Integrated Into an Existing Brewery?
Adding used equipment requires careful planning.
Before installation, check:
- Floor space
- Tank height
- Door access
- Electrical requirements
- Glycol capacity
- Pump compatibility
- Piping connections
A fermentation tank must work together with the existing brewhouse, kettle, pumps, and storage system.
For example, adding multiple tanks may require more cooling power. A brewery should confirm whether the current glycol system can support the additional load.
A complete evaluation prevents unexpected problems after installation.
Where Can You Find Used Fermentation Tanks for Sale?
Used fermentation tanks are commonly available through:
- Brewery equipment dealers
- Brewery closures
- Equipment auctions
- Industry marketplaces
- Manufacturer inventory programs
When looking at used fermentation tanks for sale, verify:
- Manufacturer information
- Serial number
- Production year
- Capacity
- Previous application
- Inspection records
Some buyers search specifically for brands such as Tiantai or other established equipment suppliers. Brand reputation can provide useful information, but actual tank condition remains the most important factor.
Should You Buy Used Fermentation Tanks or New Stainless Steel Tanks?
The decision depends on your production goals.
Choose used tanks when:
- Budget is limited
- Quick expansion is needed
- The tank condition is verified
- Modifications are acceptable
Choose new tanks when:
- Building a new brewery
- Requiring custom dimensions
- Expanding long term
- Needing guaranteed compatibility
For breweries planning long-term growth, customized equipment often provides better value because the entire system can be designed together.
Our team provides customized stainless steel brewing systems, fermentation tanks, brewhouses, and turnkey brewery solutions. We help global B2B customers select equipment based on capacity, layout, beverage type, and future expansion.
Frequently Asked Questions
Are used stainless steel fermentation tanks safe for beer production?
Yes, used stainless steel fermentation tanks can be suitable if they pass inspection, cleaning, pressure checks, and compatibility testing.
What is the difference between a fermenter and a fermentation tank?
A fermenter is another name for a fermentation tank. Both refer to a vessel where yeast converts sugars into alcohol during fermentation.
How long do stainless steel fermentation tanks last?
With proper maintenance, stainless steel tanks can operate for many years. Lifespan depends on material quality, cleaning practices, and operating conditions.
Can used fermentation tanks be customized?
Yes. Some modifications are possible, such as changing fittings, valves, or controls. However, major changes may increase costs.
Are new fermentation tanks better than used fermenters?
New tanks provide customization and manufacturer support, while used tanks may offer lower initial costs. The best choice depends on your brewery requirements.
Key Points to Remember
- Used stainless steel fermentation tanks can reduce initial investment but require careful inspection.
- Check material, pressure rating, cooling jacket, valves, and maintenance history before buying.
- A fermentation tank must match your brewhouse capacity and production schedule.
- Used fermenters may work well for expansion, but customized new tanks provide better long-term planning.
- Stainless steel design, sanitation, and temperature control are critical for beer quality.
- Working with an experienced brewery equipment manufacturer helps ensure the right tank solution for your project.
Brewery System Design: Layout Choices That Change Cost
Nancy Shang | Founder and CEO, MICET | Published September 18, 2026
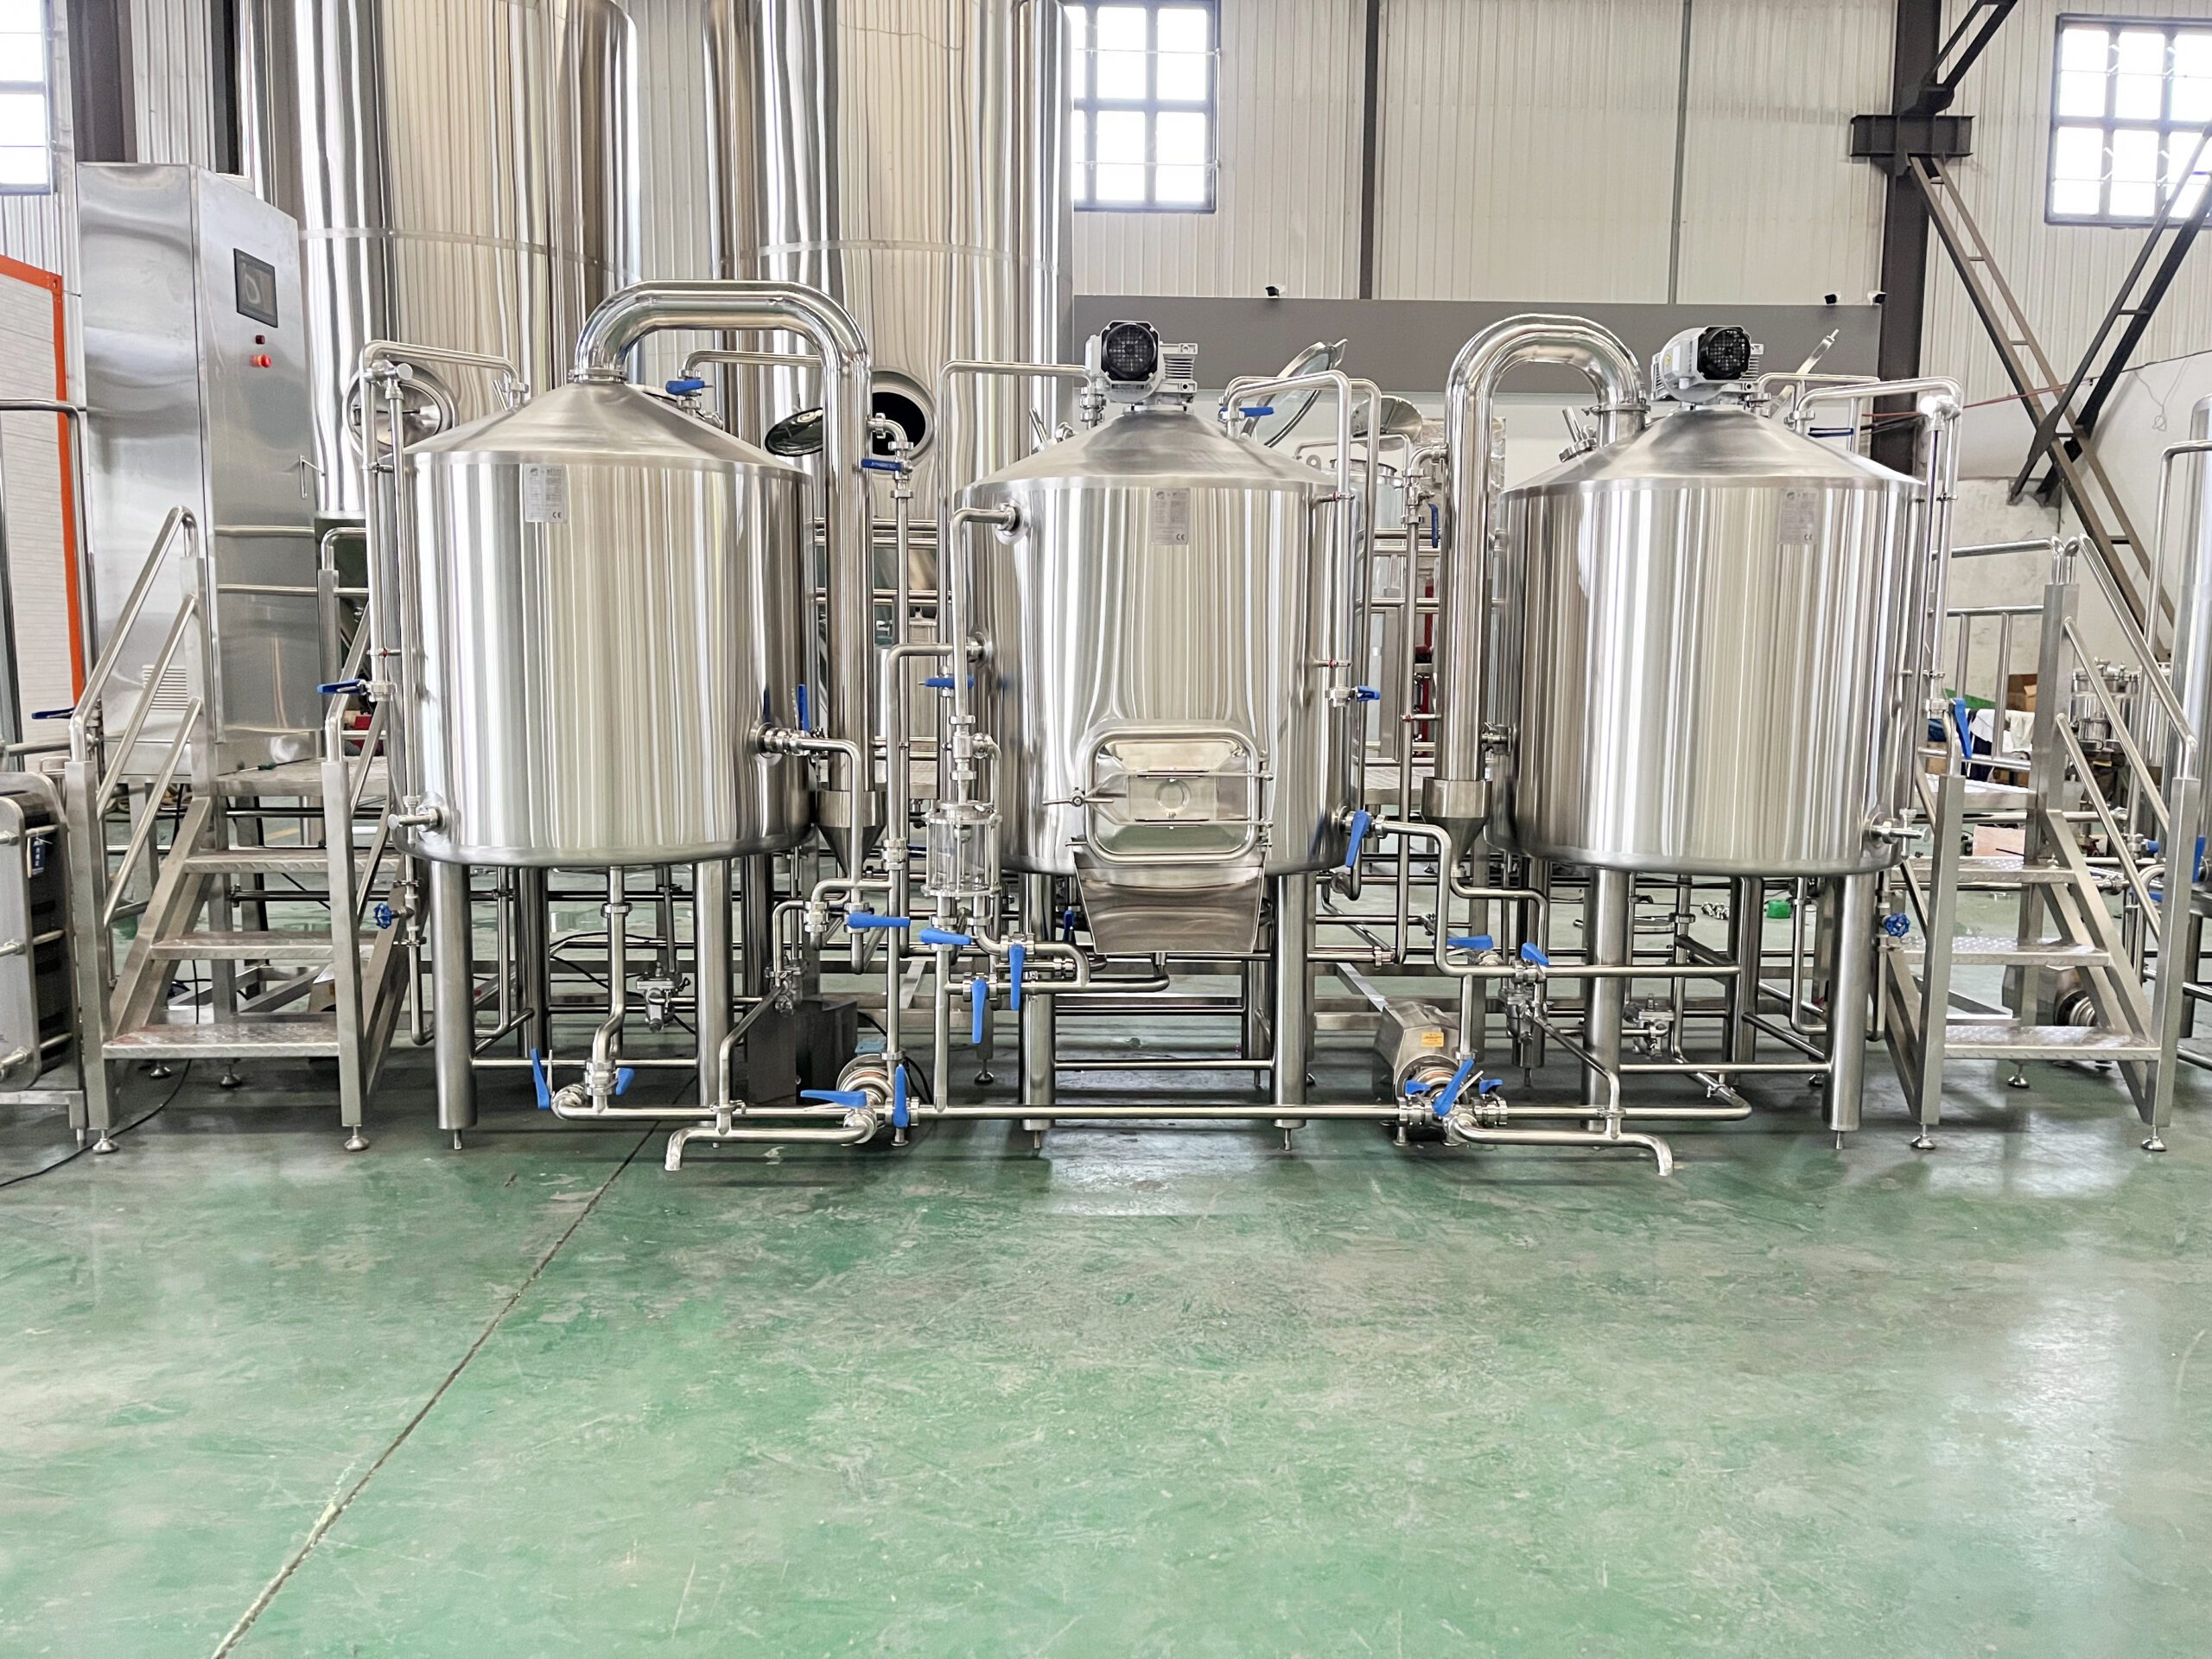
rewhouse layout — 2-vessel, 3-vessel, or 4-vessel — decides more than brew day speed: it sets your floor footprint, batch cycle time, and how easily you can add capacity later. MICET’s published used brewhouse package covers a 3-vessel configuration from 2–10 BBL. Here’s how vessel count actually changes cost and expansion.
Vessel Count at a Glance
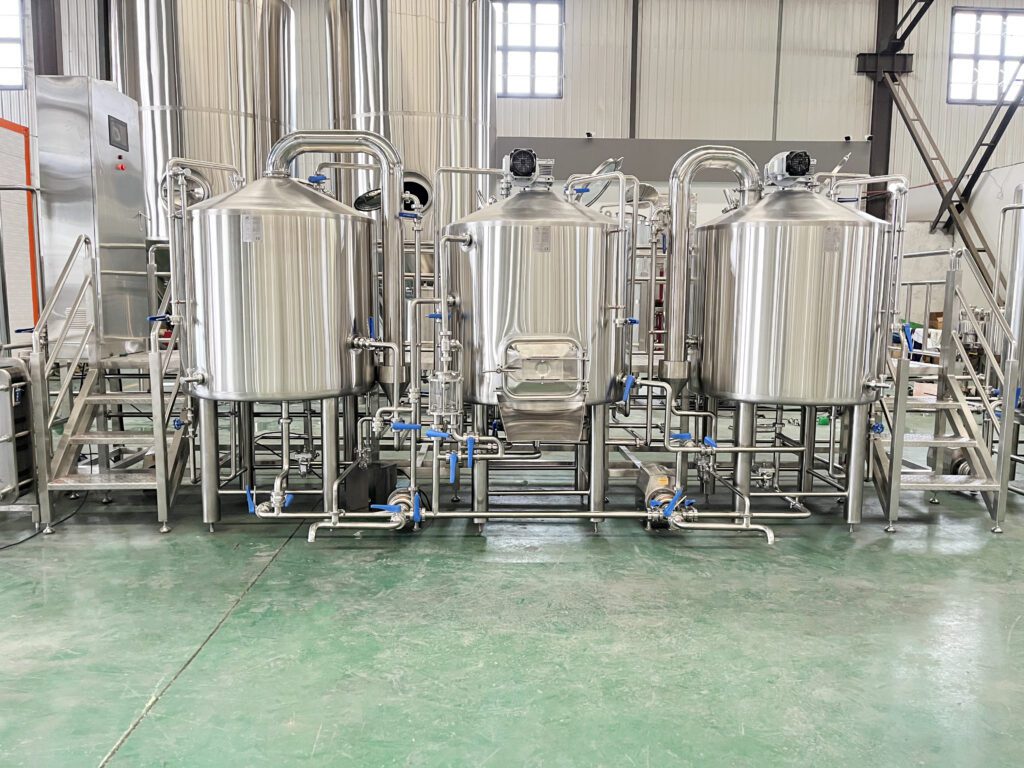
| 2-Vessel | 3-Vessel | 4-Vessel | |
| Typical role | Mash/lauter combined + kettle/whirlpool combined | Separate mash tun, kettle, and HLT (or separate lauter) | Separate mash tun, lauter tun, kettle, and whirlpool |
| Common capacity range | Nano to small pilot systems | Nano through mid-size craft (MICET’s used package: 2–10 BBL) | Mid-size craft through larger production |
| Floor footprint | Smallest — fewer tanks, fewer connections | Moderate | Largest — one more vessel plus associated piping |
| Batch cycle time signal | Slower per batch, since one vessel does double duty (mash/lauter, then cleaned for kettle/whirlpool) | Faster than 2-vessel, since mash and boil steps don’t compete for the same tank | Fastest cycle time of the three, since whirlpool separation frees the kettle sooner |
| Best fit for | Startups minimizing capex and footprint over throughput | Craft breweries balancing footprint against production speed | Breweries running hop-heavy recipes or targeting higher batch frequency |
2-Vessel Systems: The Nano and Pilot Default
A 2-vessel brewhouse combines mash and lauter functions in one tank and boil/whirlpool functions in a second. It’s the layout most nano and pilot operations start with, because it needs the least floor space and the fewest connections to plumb and maintain.
The tradeoff shows up on brew day, not on the price tag. Since the same vessel handles two sequential steps, that tank has to be cleaned and reset between mash-out and boil, which stretches total brew day length compared to a layout where those functions run in parallel-capable, dedicated vessels. For a brewer running one or two batches a week, that added cycle time rarely matters. For a brewery pushing toward daily batches, it becomes the bottleneck.
3-Vessel Systems: Where MICET’s Standard Used Brewhouse Package Lands
MICET’s published used brewery equipment line is a 2–10 BBL compact brewhouse configuration built around a mash tun, kettle, and hot liquor tank (HLT) as a set — a 3-vessel arrangement — with pumps, a heat exchanger, and a control panel included in the package.
Splitting mash and kettle functions into separate vessels means mash-out on one tank doesn’t hold up the boil on another; the HLT keeps hot water staged and ready rather than competing for space with the mash process. That’s the main reason 3-vessel layouts dominate the craft segment between nano and mid-size production — the footprint increase over a 2-vessel system is real, but modest compared to the cycle-time gain.
What MICET’s current used inventory listing doesn’t itemize is a separate lauter tun as a fourth vessel option within this package — the published configuration is fixed at mash tun, kettle, and HLT. A brewery wanting a dedicated lauter tun on top of this base package should confirm whether that’s available as an add-on or requires a different configuration entirely.
4-Vessel Systems: When a Separate Whirlpool Earns Its Footprint
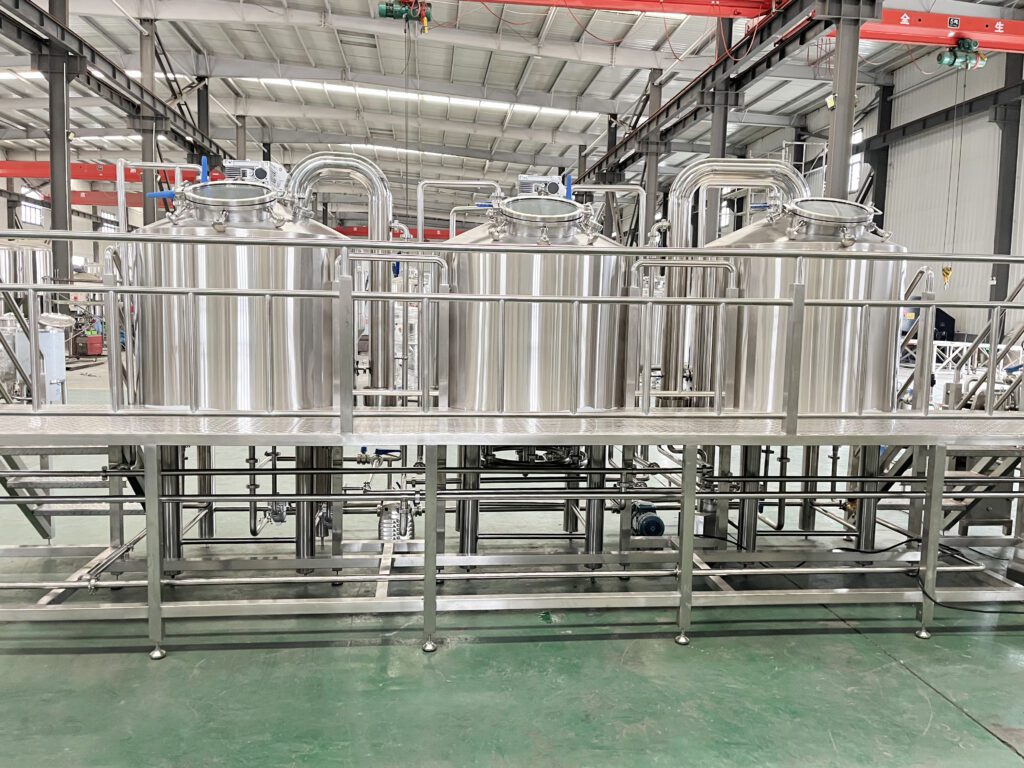
A 4-vessel layout adds a dedicated whirlpool to the mash tun, lauter tun, and kettle. The whirlpool’s job is separating hop and protein trub from the wort after the boil, and running it as its own vessel means the kettle empties and resets faster than it would if whirlpooling happened inside the kettle itself.
That speed advantage matters most for hop-heavy styles — IPAs and other recipes with large late-addition hop charges generate more trub, and a combined kettle/whirlpool vessel takes longer to settle and clear between batches. For a brewery running a hop-forward lineup at higher batch frequency, the extra vessel and floor space typically pay for themselves in throughput. For a brewery with a lighter, less hop-intensive recipe book, the fourth vessel adds cost and footprint without a matching return.
Footprint and Ceiling Height: The Constraint Vessel Count Doesn’t Solve Alone
Vessel count answers the “how many tanks” question, but two brewhouses with the same vessel count can still need very different rooms. Ceiling height matters as much as floor space, since kettles and whirlpools need clearance above them for venting and access, and a gravity-fed layout (where wort moves downward between vessels via height difference rather than pumps alone) needs more vertical clearance than a fully pumped system running on one level.
A brewery converting a retail storefront or existing warehouse bay often has a fixed ceiling height before vessel count ever enters the conversation. In that scenario, the ceiling constraint can rule out a gravity-fed 3- or 4-vessel layout regardless of how much floor space is available, pushing the decision toward a pumped configuration instead.
Capex Signals vs. Published Price Bands: What MICET’s Numbers Actually Cover
| Tier | Published Price Range | What It Includes |
| Microbrewery equipment | 30,000–80,000 USD | System-level bundle; vessel count not broken out separately |
| Commercial brewery equipment (10 BBL minimum) | 50,000–80,000 USD | System-level bundle; vessel count not broken out separately |
| Fermentation, packaging, and other add-on equipment | Not published | Quote required |
Both published ranges are bundle-level figures, not per-vessel breakdowns. That means the price difference between a 2-vessel and a 3-vessel system at the same capacity isn’t separated out in MICET’s available pricing material — a brewery comparing layouts on cost needs to request quotes for each specific configuration rather than assuming a fixed dollar-per-vessel increment applies across the published range.
The Misconception: More Vessels Isn’t Automatically More Capacity
A common assumption is that adding vessels increases batch size. It doesn’t — vessel count changes cycle time and workflow, not the volume of a single batch. A 4-vessel 10 BBL system still produces 10 BBL per batch, the same as a 2-vessel 10 BBL system. What changes is how many batches that brewhouse can realistically run in a week, since separating functions into dedicated vessels reduces the downtime between batches.
Breweries chasing higher output sometimes add vessels expecting bigger batches and end up with the same batch size run more frequently instead. That’s not a bad outcome if throughput was the actual goal, but it’s worth naming the difference before committing capex to a layout change.
Expansion Path: Retrofitting vs. Starting With Headroom
A brewery starting on a 2-vessel system can generally retrofit toward a 3-vessel layout later by adding a dedicated kettle or HLT, provided the original room has space and utility connections for it. Going from 3-vessel to 4-vessel by adding a whirlpool is usually a smaller retrofit, since it typically fits into existing piping runs more easily than a full mash/lauter split does.
The harder retrofit is capacity, not vessel count — swapping a 5 BBL mash tun for a 10 BBL one usually means replumbing connections sized for the smaller vessel, not just dropping in a bigger tank. Breweries planning to double capacity within a few years often find it cheaper to start with larger vessels running under-filled than to retrofit capacity later, even though the upfront footprint and price are higher.
Certification Note
MICET holds a PED Verification (certificate 3N231110.SICS093, issued by Ente Certificazione Macchine Srl, valid through November 9, 2028) covering brewing equipment, beer equipment, brewery equipment, and pressure vessels under the EU’s Pressure Equipment Directive 2014/68/EU, tested to EN 1626:2008. That verification sits at the organization and product-line level. On the used brewhouse product page specifically, certification is referenced only generically as “ASME/CE” craftsmanship, without a registration number or issuing body — buyers who need documentation for their own jurisdiction should request the specific unit’s paperwork before purchase rather than relying on the general reference.
Before You Commit to a Layout: 4 Questions to Answer
- What’s your target batch frequency, not just batch size — weekly, daily, or somewhere between?
- What does your recipe lineup actually demand — is trub load from hop-heavy styles significant enough to justify a dedicated whirlpool?
- What’s your ceiling height and floor footprint, confirmed with actual measurements rather than an assumed “standard” room?
- What’s your 3-year capacity plan — is it cheaper to size vessels for future volume now, or to plan a defined retrofit path later?
FAQ
Q: Does adding a vessel to a brewhouse increase batch size?
A: No. Vessel count affects cycle time and workflow speed, not the volume of a single batch. A 10 BBL system produces 10 BBL per batch whether it’s a 2-vessel or 4-vessel layout — more vessels mean the brewhouse can typically run more batches per week, not bigger ones.
Q: What vessel configuration does MICET’s used brewhouse package include?
A: The published 2–10 BBL used brewery equipment package is a 3-vessel configuration — mash tun, kettle, and hot liquor tank — with pumps, a heat exchanger, and a control panel included.
Q: Is a 4-vessel system worth the extra footprint?
A: It depends on the recipe lineup and target batch frequency. Hop-heavy styles with significant trub load and breweries targeting higher batch frequency tend to see the clearest return on a dedicated whirlpool. A lighter, less hop-intensive lineup often doesn’t need it.
Q: Does MICET’s certification cover pressure vessel compliance for used brewhouse equipment?
A: MICET’s PED Verification (3N231110.SICS093) covers brewing and pressure vessel equipment at the organization and product-line level. The used brewhouse product page itself references certification only generically as “ASME/CE” without a specific registration number, so individual-unit documentation should be confirmed directly before purchase.
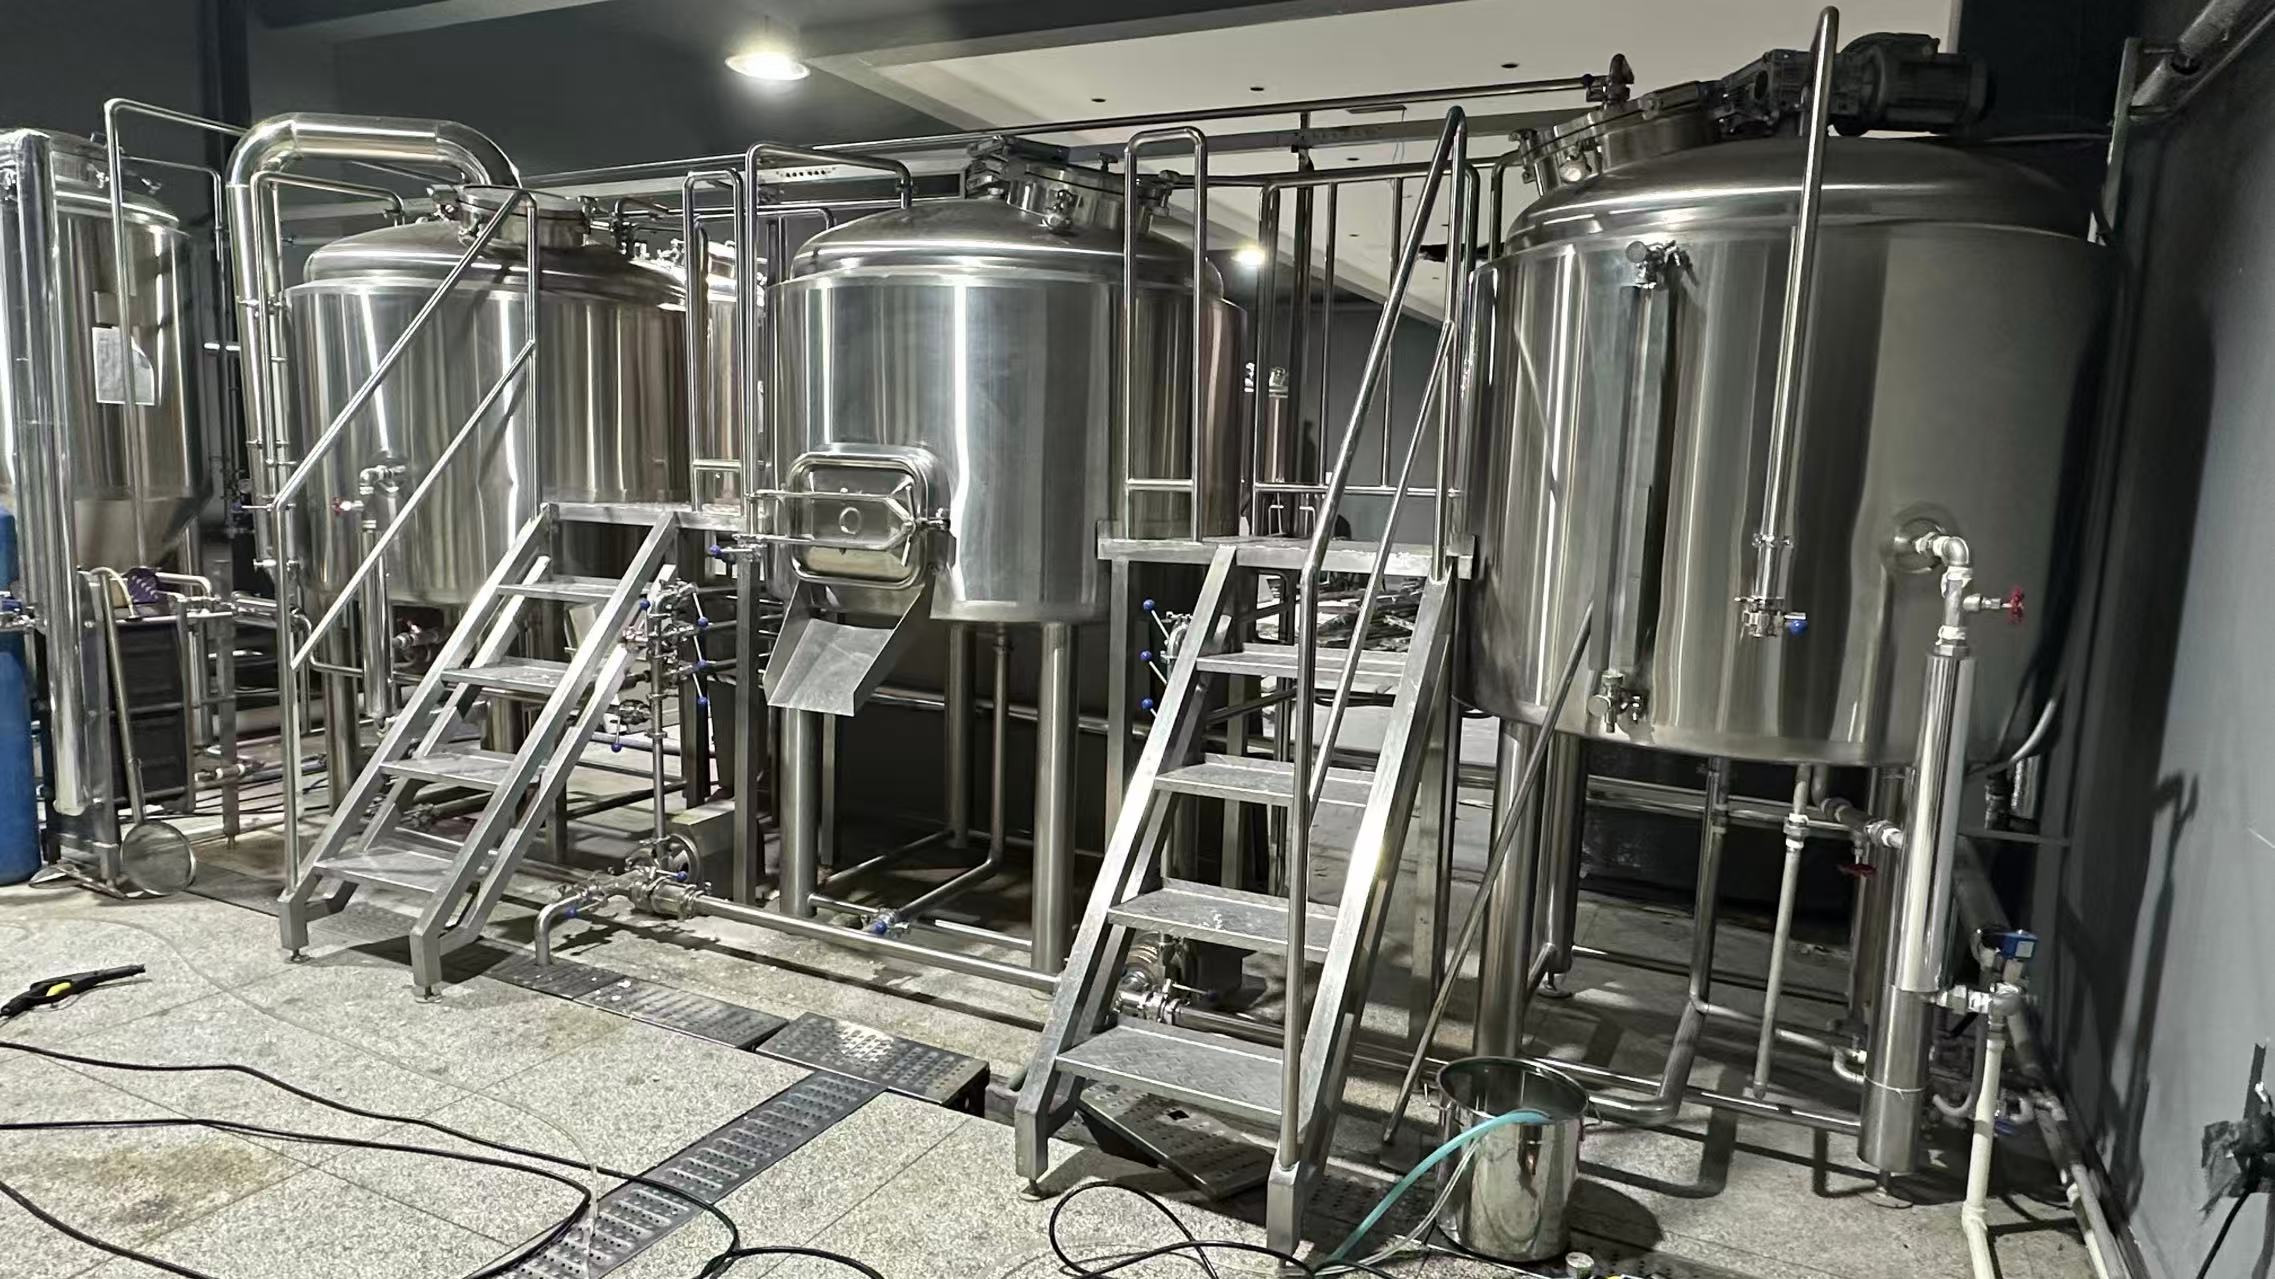
Used 1000L Three-Vessel Craft Beer Brewing Equipment for Sale
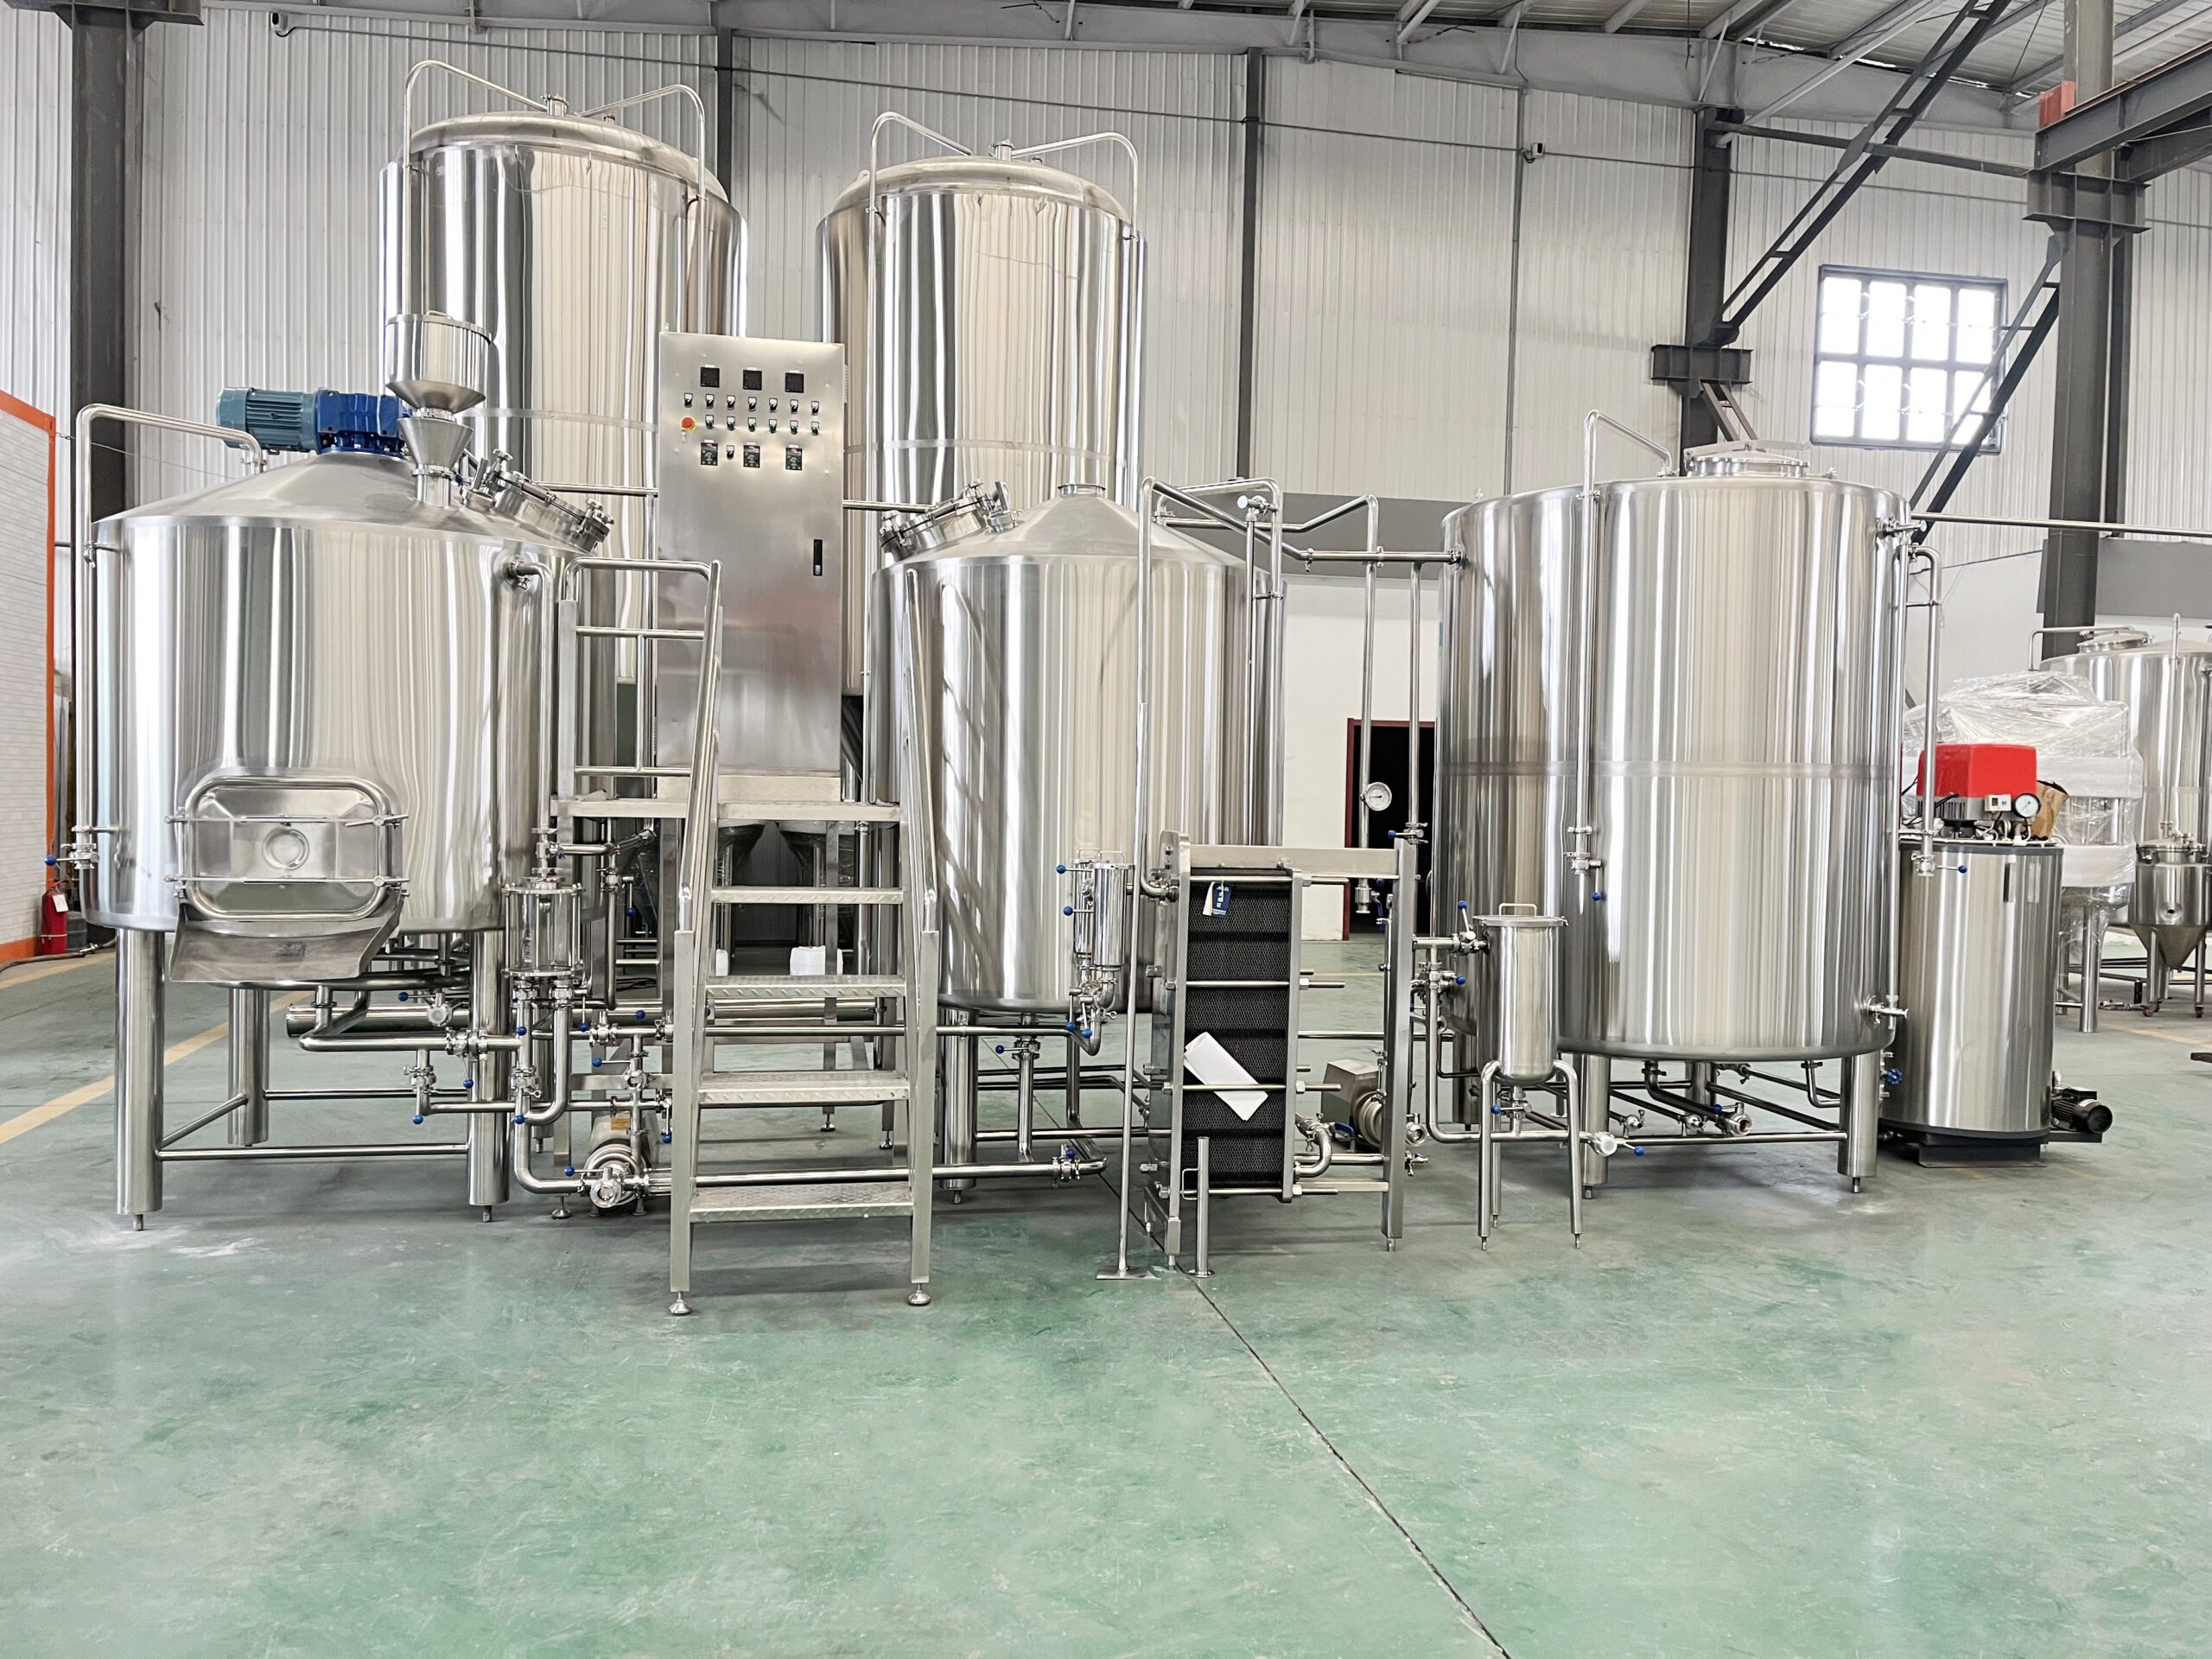
A nearly new 1000L three-vessel craft beer brewing system, manufactured in 2025, is now available for sale. This complete used brewery equipment package features a three-vessel brewhouse, 11 fermentation tanks, a dedicated cooling system, water treatment equipment, and essential brewing accessories.
With a high level of automation and a comprehensive configuration, this system is suitable for craft breweries, brewpubs, restaurants, and commercial beer production projects looking for a complete 1000L brewing solution.
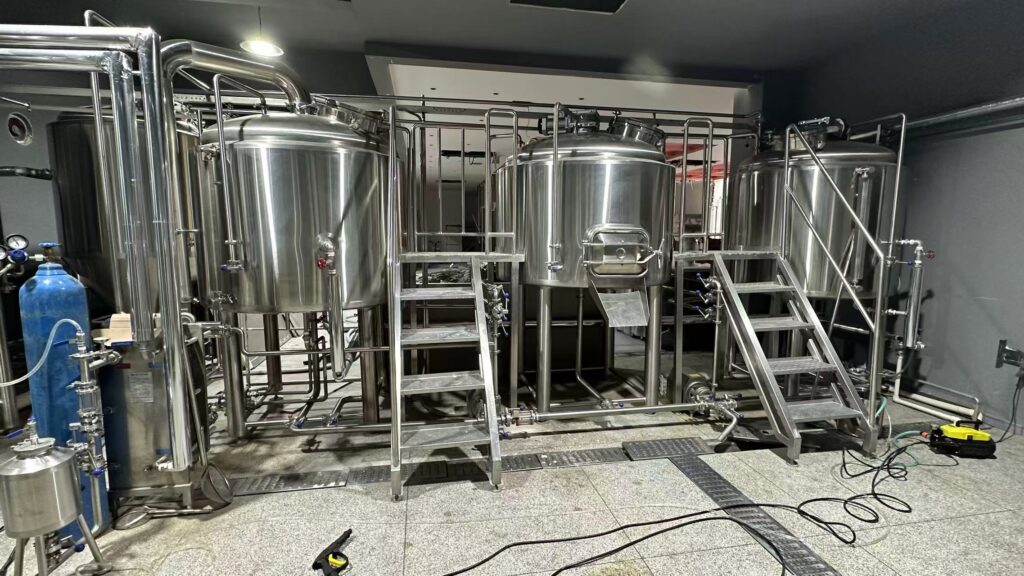
1000L Three-Vessel Brewhouse System
The brewhouse is designed with a three-vessel configuration and equipped with glass viewing manways on all three vessels, allowing operators to observe the brewing process more conveniently.
The mashing system features automatic step-temperature control, supporting programmed temperature increases during different mashing stages. This helps improve process consistency and operational convenience.
The lauter tun is equipped with an automatic raking and spent-grain discharge system, reducing manual handling during lautering. An 8 m² plate heat exchanger, hop filter, and yeast addition tank are also included to support the subsequent wort cooling and yeast pitching processes.
Brewhouse Configuration
| Item | Specification |
|---|---|
| Equipment Type | Used 1000L Three-Vessel Brewery System |
| Brewhouse Configuration | Three-Vessel System |
| Viewing Manways | Glass Viewing Manways on All Three Vessels |
| Mashing Control | Automatic Step Temperature Ramping |
| Lauter Tun | Raking System with Automatic Spent-Grain Discharge |
| Plate Heat Exchanger | 8 m² |
| Hop System | Hop Filter |
| Yeast System | Yeast Addition Tank |
| Control Cabinet | Floor-Standing Stainless Steel PLC Control Cabinet |
| Variable Frequency Drives | 3 Units |
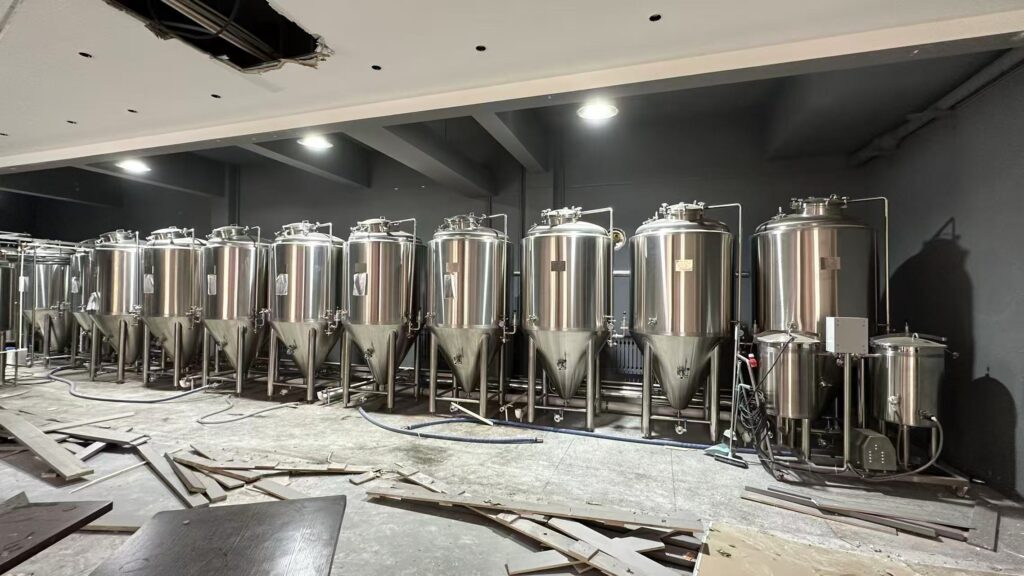
11 × 1000L Stainless Steel Fermentation Tanks
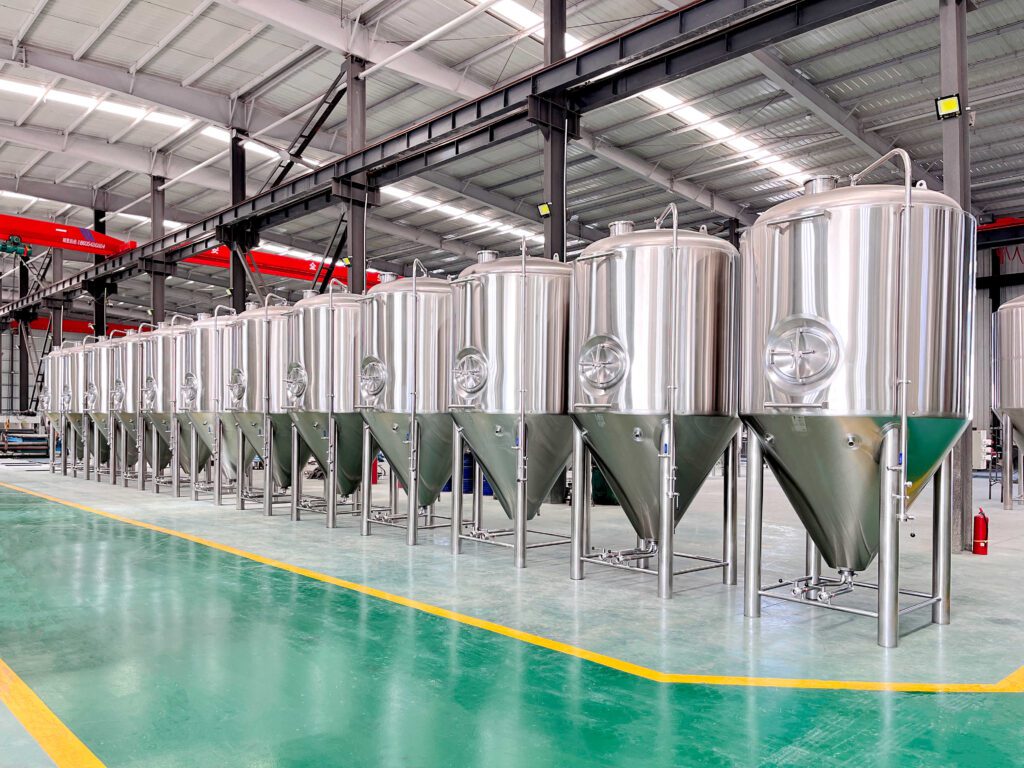
The fermentation section includes 11 units of 1000L stainless steel fermentation tanks with top manways. This configuration provides sufficient fermentation capacity for multi-batch production and flexible scheduling of different beer varieties.
Each fermenter is equipped with a dry-hopping port and a water-seal valve, supporting dry-hopping operations and related craft brewing processes. The top manway design also facilitates inspection, cleaning, and routine maintenance.
Cooling and Water Treatment Systems
To support wort cooling and fermentation temperature management, the system includes a 2500L ice water tank and a 10 HP Maigebeit cooling unit. These components provide cooling support for the brewing and fermentation stages.
The package also includes a 1000L raw water tank, a 1000L purified water tank, and a 1T/h water treatment system. Together, these components provide a practical water storage and treatment solution for brewing operations.
|
Item |
Specification |
|---|---|
|
Fermentation Tanks |
1000L Top-Manway Fermenters |
|
Fermenter Quantity |
11 Units |
|
Fermenter Accessories |
Dry-Hopping Port and Water-Seal Valve |
|
Ice Water Tank |
2500L |
|
Cooling Unit |
10 HP Maigebeit |
|
Raw Water Tank |
1000L |
|
Purified Water Tank |
1000L |
|
Water Treatment Capacity |
1T/h |
Complete Auxiliary Equipment
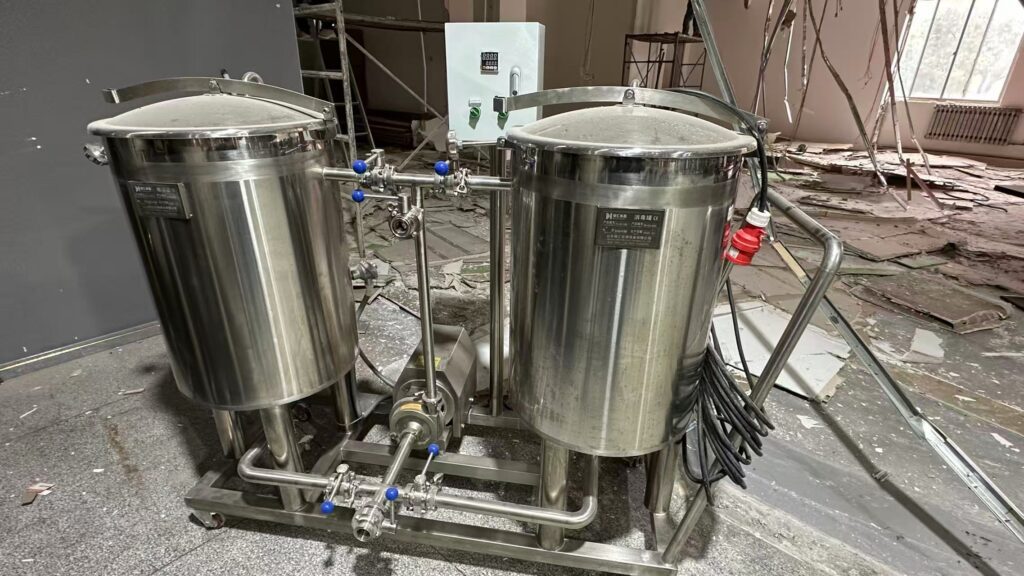
In addition to the main brewing, fermentation, and cooling systems, this used brewery package includes a stainless steel grain mill and a 100L dual-tank CIP cleaning cart. The complete configuration helps support raw material preparation, equipment cleaning, and routine brewery operations.
The stainless steel PLC control cabinet provides centralized control for the brewing system, while the three variable frequency drives support adjustable operating speeds for compatible equipment.
Suitable for Commercial Craft Brewing Projects
This 2025-manufactured nearly new 1000L three-vessel craft beer brewing system offers a comprehensive equipment configuration for breweries seeking to establish or expand commercial production capacity.
With its automatic step mashing control, automatic spent-grain discharge, multiple fermentation tanks, cooling system, and water treatment equipment, the package provides a practical foundation for a complete craft beer production line.
For customers looking for used brewery equipment with a relatively recent manufacturing date and extensive supporting equipment, this 1000L system is worth considering. Equipment condition, technical specifications, and availability can be confirmed according to the buyer’s requirements.

Wholesale Brewing Equipment: OEM Options for Distributors
Nancy Shang | Founder and CEO, MICET | Published September 17, 2026
Sourcing wholesale brewing equipment as a distributor means evaluating package contents, MOQ tiers, certification scope, and after-sales handoff — not just unit price. This guide walks through what MICET publishes on each of those points, where the gaps are, and what to ask before signing a regional agreement.
What “Wholesale Brewing Equipment” Means for a Distributor, Not an End User
A brewery owner buying one 10 BBL system cares about brew day performance. A distributor buying wholesale brewing equipment cares about something different: whether the manufacturer can support ten of those systems shipped to ten different customers, each with their own installation timeline, warranty claim, and spare parts request.
That shift changes which questions matter. Unit specs still matter, but they sit alongside questions a single-unit buyer never asks — pricing tiers by volume, documentation the distributor can hand to their own customer, and who answers the phone when a compressor fails in month eight.
OEM vs. ODM: Two Different Deals, Not Interchangeable Terms
OEM (original equipment manufacturer) arrangements typically mean the distributor sources a manufacturer’s standard design and resells it, sometimes under their own brand name on the nameplate. ODM (original design manufacturer) arrangements go further — the manufacturer adjusts the design itself to a distributor’s specifications before production.
MICET’s published catalog describes standard configurations (used brewhouse packages, fermentation tanks, kombucha and distillery lines) rather than a formal OEM/ODM program with defined tiers. Distributors evaluating white-label or private-label options should treat this as an open question to raise directly rather than an assumed service — the resource material behind this article doesn’t confirm branding terms, minimum customization thresholds, or nameplate policy.
The 2–10 BBL Package: What’s Actually Included
For distributors reselling into the craft and nano-brewery segment, MICET’s used brewery equipment line covers 2–10 BBL compact brewhouse configurations. The published package includes:
- Mash tun, kettle, and hot liquor tank (HLT) as a set
- Pumps
- Heat exchanger
- Control panel
What isn’t itemized at this tier: fermentation tanks, packaging lines, and CIP systems are separate line items, not bundled into the base brewhouse package by default. A distributor quoting a “complete turnkey” system to their own customer needs to confirm which additional equipment gets added and priced separately, since the 2–10 BBL brewhouse figure alone won’t cover a full production setup.
MOQ Tiers: What’s Published and What You’ll Need to Ask For
Minimum order quantities for wholesale brewing supplies aren’t published in MICET’s available material. Distributors accustomed to seeing tiered MOQ pricing from other equipment categories should not assume the same structure applies here without confirming it directly — this is a genuine information gap in the source data behind this article, not an oversight in this guide.
What is documented is the scale of the operation behind the equipment: a 10,000+ m² certified production base and 22 years of combined technical engineering experience on the team. Neither figure substitutes for an MOQ number, but both are relevant context when a distributor is deciding whether a manufacturer can handle a multi-unit order on a compressed timeline.
Certification Distributors Need for Their Own Market
This is where distributors run into the most friction, because certification schemes are regional and a certificate covering one market doesn’t automatically satisfy another.
MICET holds a PED Verification (certificate 3N231110.SICS093, issued by Ente Certificazione Macchine Srl, valid through November 9, 2028) covering brewing equipment, beer equipment, brewery equipment, and pressure vessels under the EU’s Pressure Equipment Directive 2014/68/EU, tested to EN 1626:2008. That certification sits at the organization and product-line level — it doesn’t automatically apply to a specific used unit pulled from resale inventory, and a distributor reselling a used system should request that unit’s individual test documentation separately.
On the used brewery equipment product page specifically, certification is referenced generically as “ASME/CE” craftsmanship, without a registration number or issuing body listed. That distinction matters for distributors targeting the US market: ASME (the American boiler and pressure vessel code) and the EU’s CE/PED scheme are not the same certification framework, and a CE-marked pressure vessel isn’t automatically ASME-compliant. Distributors selling into ASME-jurisdiction markets should confirm ASME-specific documentation exists for the actual units they’re ordering, not assume CE coverage extends there.
Pricing Structure by Tier
| Package Tier | Published Range |
| Microbrewery equipment | 30,000–80,000 USD |
| Commercial brewery equipment (10 BBL minimum) | 50,000–80,000 USD |
| Fermentation, kombucha, distillery, wine, and packaging lines | Not published — quote required |
For a distributor building a resale price list, only the two brewhouse tiers above have a published floor and ceiling. Everything outside the brewhouse category needs a direct quote before it can be priced for a customer, and that quote request should specify capacity and configuration rather than assuming the brewhouse ranges scale proportionally to other equipment types.
Where MICET Already Has Agents — and Where That Leaves Room
MICET operates service centers or agent offices in France, Australia, Canada, Argentina, and Chile, with confirmed sales agents or distributors already active in Canada, the USA, the UK, France, Georgia, Italy, South Africa, India, Argentina, and Chile. A distributor evaluating a new territory should check this list first — a region with an existing agent means a different conversation (possible sub-distribution or coordination) than a region with no coverage yet, which is a more straightforward greenfield discussion.
After-Sales Support: Who Handles the Warranty Call?
MICET advertises 24/7 after-sales service and more than 20 sales representatives across different countries. What isn’t specified in the available material is how warranty and service responsibility splits between MICET directly and a regional distributor once equipment is installed — whether the distributor becomes the first point of contact for their own customers, or whether service requests route back to MICET’s team regardless of territory. This is a contractual detail distributors need to settle before finalizing a regional agreement, not something to infer from the general after-sales claim alone.
The Compliance Gap Most Distributors Miss First
The most common mistake in wholesale brewing equipment sourcing isn’t a pricing error — it’s assuming a supplier’s published certification covers every export market a distributor plans to sell into. A manufacturer with solid EU documentation can still leave a distributor exposed in a market that requires ASME, UL, or a national equivalent that hasn’t been tested against. The fix isn’t complicated, but it does take an extra step most distributors skip under deadline pressure: confirm certification scope against each target country’s actual import and installation requirements before quoting a customer, not after the equipment ships.
Getting Set Up as a Regional Partner: 6 Steps
- Identify whether your target territory already has a confirmed MICET agent or service center, using the coverage list above.
- Request current pricing for the specific package tier and capacity range you plan to resell.
- Ask directly about MOQ, OEM/ODM terms, and any private-label or nameplate options — none of these are published, so they need a direct answer before you build a resale price list.
- Confirm certification scope for your target market specifically, including whether ASME or another regional equivalent is available or needs separate arranging.
- Clarify the after-sales service split in writing — who handles first-line support, warranty claims, and spare parts requests once equipment reaches your customer.
- Request documentation you can hand to your own customers: installation manuals, layout drawings, and individual-unit test records where applicable.
FAQ
Q: Does MICET offer white-label or private-label branding for distributors?
A: This isn’t confirmed in MICET’s published material. Distributors interested in nameplate or branding options should raise it directly rather than assume it’s a standard offering.
Q: What’s the minimum order quantity for wholesale brewing equipment?
A: MOQ figures aren’t published. Distributors should request tier-specific MOQ information directly when discussing a regional agreement.
Q: Is MICET’s CE/PED certification enough for the US market?
A: Not automatically. The published PED Verification (3N231110.SICS093) covers the EU’s Pressure Equipment Directive scheme. ASME, the US pressure vessel code, is a separate framework, and the used equipment line’s certification is referenced only generically as “ASME/CE” without a registration number — distributors targeting ASME-jurisdiction markets should confirm specific documentation before quoting customers there.
Q: Can MICET dispatch technicians to support installation in a new territory?
A: MICET advertises 24/7 after-sales service and a team of more than 20 sales representatives across different countries, but on-site technician dispatch terms for a specific territory aren’t detailed in the available material and should be confirmed directly for the region in question.
Cylindroconical Fermenter Design: Geometry Tradeoffs
Nancy Shang | Founder and CEO, MICET | Published September 16, 2026
A cylindroconical fermenter’s performance hinges on four interlocking choices: cone angle, height-to-diameter ratio, jacket zoning, and racking arm height. Get the cone angle wrong and yeast won’t drop cleanly; skip jacket zoning and cooling lags during high-krausen fermentation. This guide breaks down each tradeoff and what MICET’s published fermenter specs actually cover.
What a Cylindroconical Fermenter Actually Is
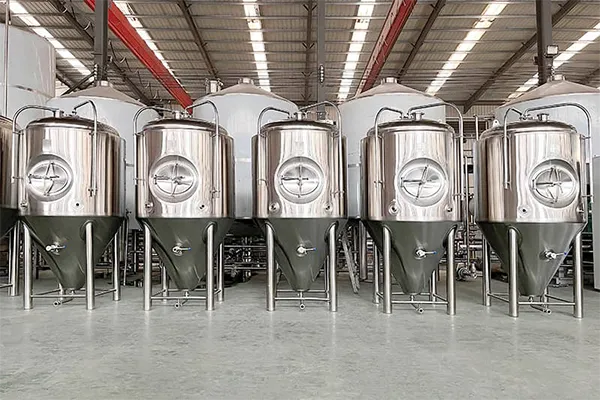
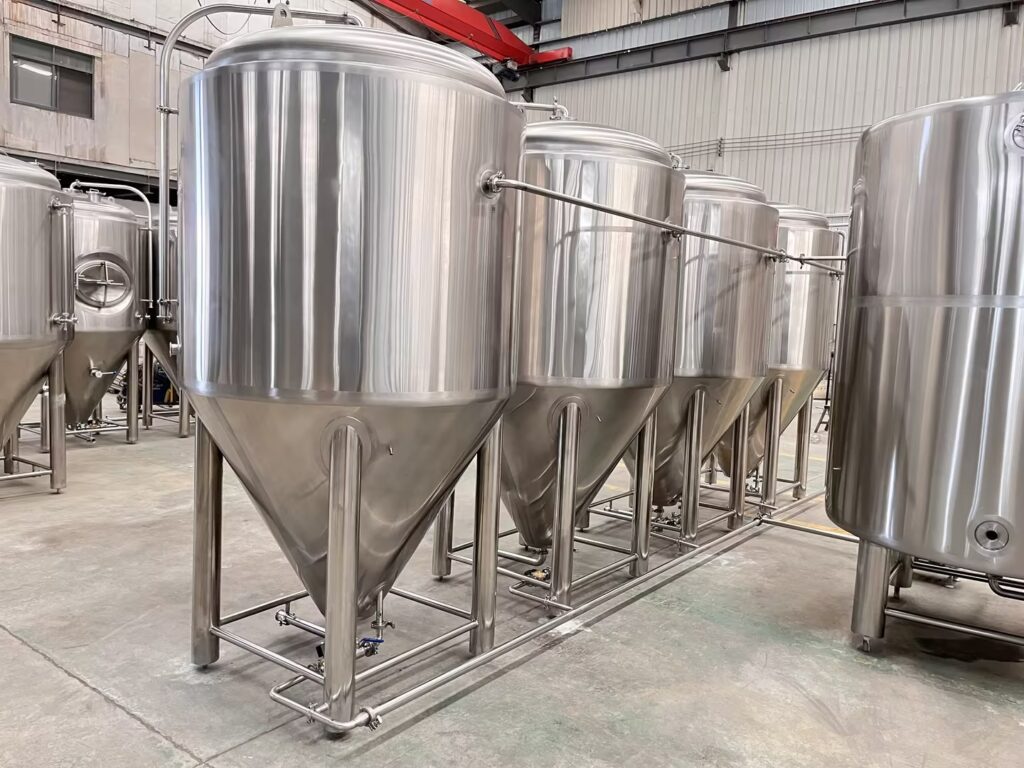
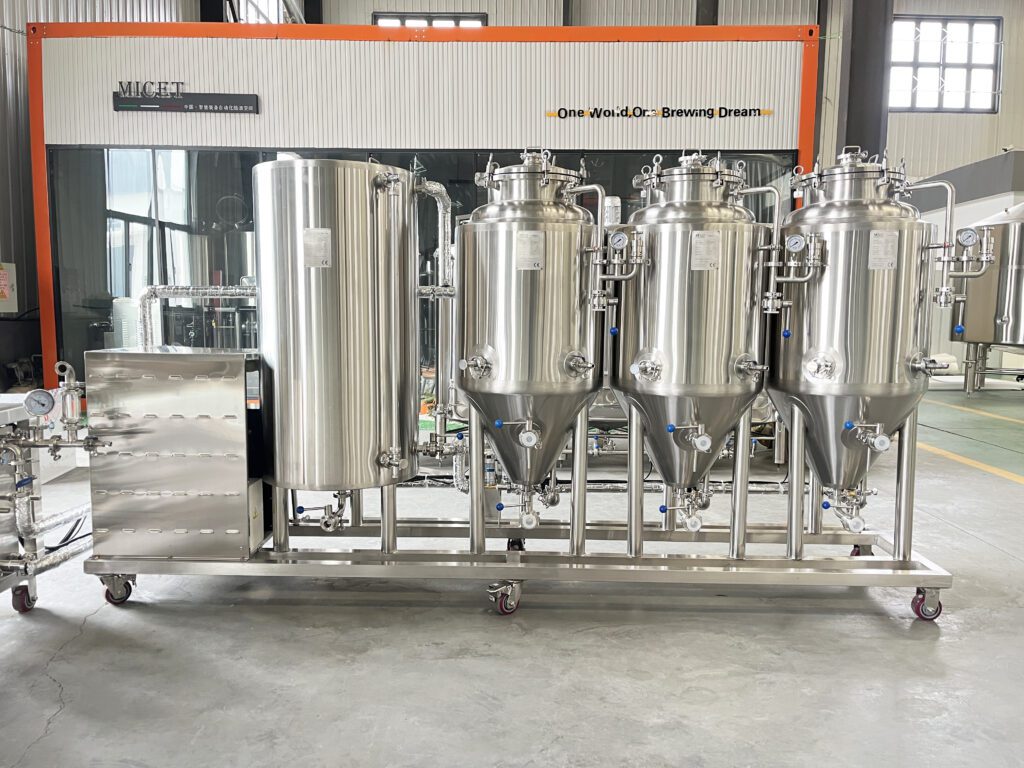
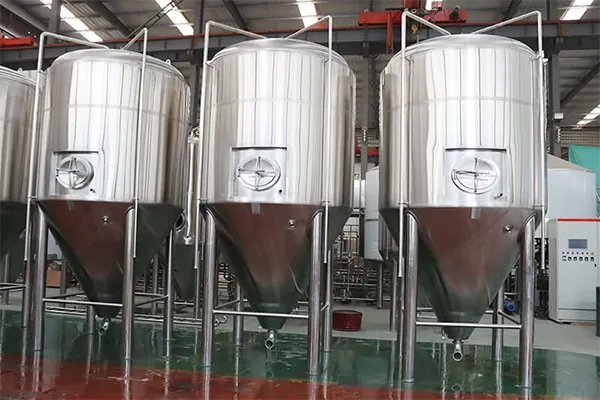
A cylindroconical fermenter (CCF) is a vertical tank with a cylindrical fermentation chamber sitting on top of a cone-shaped base. The shape does two jobs at once: it holds beer during active fermentation, and its cone geometry lets yeast and trub settle to a single low point instead of spreading across a flat floor. That single point is where the harvest valve sits.
The tradeoff is baked into the shape itself. A tank optimized purely for yeast drop-out — a narrow, steep cone — costs more per liter of usable volume than a shallow-cone design built for storage efficiency. Every dimension decision downstream of the cone angle is a compromise between these two goals.
Cone Angle: The 60° Default and When It’s Wrong
Most commercial CCFs use a cone angle somewhere between 60° and 70° from horizontal. At that slope, sediment slides toward the harvest valve under gravity alone, without mechanical agitation. Go shallower than roughly 45° and material starts sticking to the cone walls instead of sliding — brewers end up rousing the tank or accepting yeast loss they didn’t plan for.
Steeper isn’t automatically better, though. A tighter cone concentrates trub and yeast into a smaller footprint, which shortens the harvest window and improves yeast viability for repitching. It also increases fabrication cost near the base, since more steel is needed to close a narrow angle without weak welds at the transition seam. For a homebrew-to-nano jump (under 1,000L), the extra cost per degree of cone steepness rarely pays for itself. For a production brewery repitching the same yeast strain across 10+ batches, it usually does.
Height-to-Diameter Ratio: The Tradeoff Nobody Explains Upfront
Height-to-diameter (H:D) ratio decides how much surface area the beer has relative to its volume, and that changes fermentation behavior more than most buyers expect going in.
A tall, narrow tank (H:D above roughly 3:1) builds more hydrostatic pressure at the bottom, which can suppress ester production in some yeast strains — useful for clean lager profiles, less useful when a brewer wants a fruity ale character. It also concentrates CO2 pressure unevenly through the fermenting wort, so temperature control has to work harder near the base than near the top.
A squatter tank (H:D closer to 1:1 or 1.5:1) fits under lower ceiling clearances and ferments with less pressure differential top to bottom, but takes up more floor footprint per liter of capacity. For a brewery converting an existing retail or warehouse space rather than building to spec, floor footprint often decides the ratio before fermentation chemistry does.
Where Does the Cooling Load Really Concentrate? Jacket Zoning
A single glycol jacket wrapped around the whole tank cools evenly in theory. In practice, fermentation generates most of its heat during high krausen — the first 24 to 48 hours — and that heat concentrates in the upper cylindrical section where yeast activity peaks, not the cone.
Multi-zone jacketing splits the cooling surface into separate glycol circuits, usually one for the upper cylinder and one for the cone, so the control system can pull heat aggressively from the active zone without overcooling the settled sediment below. Single-zone jackets are cheaper to fabricate and simpler to plumb, but they force a compromise: set the glycol temperature for the hot zone and the cone runs colder than necessary, or set it for average conditions and peak krausen runs warmer than the recipe calls for.
For most fermenters under 20 BBL running standard ale or lager schedules, single-zone jacketing is adequate. Multi-zone control earns its added plumbing complexity mainly on larger tanks or where a brewery is running temperature-sensitive strains across variable batch sizes.
Racking Arm Placement Isn’t an Afterthought
The racking arm — the fitting used to draw finished beer off the tank without disturbing settled sediment — sits above the cone’s lowest point, not at it. Its exact height above the transition seam determines how much clear beer a brewer can pull before trub starts coming through, and how much product gets left behind or has to be filtered separately.
Set too low, and the arm draws sediment into the racked beer during the final draw. Set too high, and usable beer volume drops because more liquid sits below the arm than the cone geometry requires. On a well-specified CCF, racking arm height is matched to the cone angle and expected sediment volume for the batch size, not bolted on at a default position regardless of tank shape.
MICET Used Fermentation Tank Specs: What’s Published and What Isn’t
MICET’s used fermentation tank inventory is published with capacity, material, and thermal specifications. Cone angle, height-to-diameter ratio, jacket zone count, and racking arm height are not part of the published catalog and are not estimated here — buyers evaluating a specific unit should request the fabrication drawing before purchase.
| Spec | Published Value |
| Capacity range | 3–5 BBL, 10 BBL, 20 BBL, 40 BBL; also 2T / 4T / 6T (2,000L / 4,000L / 6,000L total; 1,800L / 3,600L / 5,400L working capacity) |
| Shell material | SUS304 stainless steel |
| Cooling | Glycol jacket |
| Insulation | Polyurethane |
| Design pressure | 0.2 MPa |
| Test pressure | 0.3 MPa |
| Cone angle | Not disclosed |
| Height-to-diameter ratio | Not disclosed |
| Jacket zone count | Not disclosed |
| Racking arm height | Not disclosed |
| Individual-unit certification | Not disclosed |
On that last row: MICET holds a Verification of Conformity for fermentation equipment (ICR/VC/HM2507146, issued by ICR Co., Ltd., under the EU Pressure Equipment Directive 2014/68/EU, tested to EN 1626:2008 and EN 10204:2004, valid through July 15, 2030). That verification applies at the organization and product-line level. It doesn’t transfer automatically to a specific used or refurbished tank on the resale floor — a used unit’s individual documentation should be confirmed separately before it factors into a purchase decision.
Standalone pricing for fermentation tanks isn’t published either. MICET’s disclosed ranges cover microbrewery systems (30,000–80,000 USD) and complete commercial systems at 10 BBL minimum (50,000–80,000 USD) — both bundle brewhouse, fermentation, and ancillary equipment rather than pricing a fermenter alone. A standalone used fermenter quote depends on capacity, condition, and current inventory, so it has to come from a direct request rather than a published number.
The Misconception That Costs Buyers Money: Steeper Isn’t Always Better
The most common mistake in fermenter selection is treating cone angle as a single “better or worse” spectrum, with steeper always winning. It doesn’t work that way for used equipment specifically.
A steep-cone tank pulled from a lager-focused brewery was likely optimized for clean, slow-dropping strains repitched many times. Installed into an ale-heavy production schedule with faster, more flocculent yeast, that same steep cone can actually cause harvest-valve clogging, because the sediment compacts faster than the smaller outlet can clear it. The geometry that made a used tank ideal for its original owner doesn’t automatically transfer to a different fermentation profile. Buyers comparing used cylindroconical tanks need the original brewery’s yeast strain and batch cadence, not just the cone angle in isolation, to judge fit.
Used vs. New: What to Verify Before You Buy
Buying a used cylindroconical fermenter trades a lower price for the responsibility of verifying geometry and condition yourself, since resale listings rarely include the original fabrication drawing. A practical pre-purchase check looks like this:
-
Request the original fabrication drawing or general arrangement (GA) sheet, including cone angle and racking arm height.
- Confirm the design and test pressure ratings against the tank’s current pressure gauge or a fresh hydrostatic test, not the nameplate alone — nameplates can outlive gasket and weld integrity.
- Inspect the jacket for glycol leaks at weld seams, particularly near the cone-to-cylinder transition, where thermal cycling stresses the joint most.
- Verify polyurethane insulation hasn’t degraded or trapped moisture, which shows up as cold spots or condensation on the outer shell during a cooling cycle.
- Ask whether the seller can provide individual-unit test documentation, separate from any manufacturer-level certification that doesn’t cover the specific tank.
New fermenters cost more but come with a documented cone angle, H:D ratio, and jacket configuration matched to the buyer’s stated fermentation profile from the start. Used units cost less and can be sourced faster, but the geometry was set for someone else’s yeast strain and batch size — the buyer inherits that decision along with the tank.
FAQ
Q: Is there one “correct” cone angle for a craft brewery fermenter?
A: No single angle works for every strain and batch size. A steeper cone (closer to 70°) speeds sediment drop-out and suits strains repitched frequently; a shallower cone (closer to 60°) trades some of that speed for lower fabrication cost. The right angle depends on yeast flocculation behavior and how often the brewery repitches, not a universal standard.
Q: Does a taller height-to-diameter ratio always mean a “better” fermenter?
A: No. A taller ratio increases hydrostatic pressure and can suppress ester production, which helps clean lager profiles but works against brewers targeting a fruitier ale character. Ceiling clearance and floor footprint also factor into which ratio actually fits a given space.
Q: If MICET holds a pressure equipment certification, does that cover every used fermenter it sells?
A: The Verification of Conformity (ICR/VC/HM2507146) is an organization- and product-line-level document, not a per-unit certificate. A specific used tank’s individual documentation and test history should be confirmed separately before purchase.
Q: How much does a used cylindroconical fermenter cost?
A: MICET doesn’t publish standalone fermenter pricing; disclosed ranges cover bundled microbrewery (30,000–80,000 USD) and 10 BBL-minimum commercial systems (50,000–80,000 USD). Contact MICET directly for a quote on a specific used fermenter capacity and condition.
Variable Capacity Wine Tanks: What Small Wineries Need
Nancy Shang | Founder and CEO, MICET Brewing | Published September 11, 2026
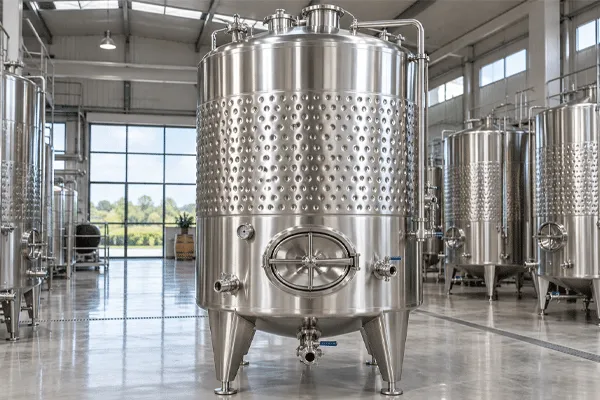
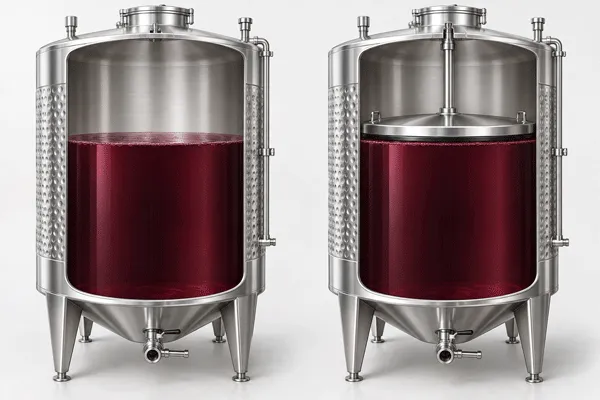
A variable-capacity wine tank uses a floating lid that drops as wine volume falls, keeping headspace minimal without racking to a smaller vessel. A fixed tank holds one nominal volume with a set headspace instead. For wineries running several small lots at once, the real tradeoff is upfront cost against fewer transfers and lower oxidation exposure.
What Is a Variable-Capacity Wine Tank?
The core mechanism is a lid — a disc, piston, or telescoping shell section — that rests directly on the surface of the wine and is sealed against the tank wall with a gasket. As wine is drawn off during racking, blending, or topping losses, the lid rides down with the liquid level instead of leaving a growing pocket of air above the wine.
Three formats show up across the market:
- Floating disc lid: a flat plate on a center post or side guides, sealed with an O-ring or wiper gasket against the tank wall.
- Telescoping shell: the tank itself is built from two or more nested cylindrical sections that collapse into each other as volume drops.
- Inflatable bladder lid: a flexible membrane inflated to press against the wine surface, adjusted by adding or releasing gas.
All three exist to solve the same problem: oxygen exposure in a partially full tank. A fixed tank at half capacity has a headspace equal to half its volume; a variable-capacity tank at the same fill level has almost none.
Variable Capacity vs. Fixed-Volume Tanks: The Practical Difference
| Factor | Fixed-Volume Tank | Variable-Capacity Tank |
| Headspace at partial fill | Grows as volume drops | Stays minimal by design |
| Typical use case | Full-batch fermentation, single-lot storage | Multi-racking cycles, blending, topping-sensitive aging |
| Upfront cost premium | Baseline | Typically 20–40% higher for equivalent nominal capacity (industry-general range; confirm current pricing with the manufacturer) |
| Cleaning complexity | Standard CIP pass | Added seal/gasket and lid-track cleaning |
| Sizing flexibility across vintages | Fixed nominal volume only | Usable across a volume range within one vessel |
Compared with typical single-SKU retailer listings — where each product page shows one fixed nominal volume per model — the sizing question for a small winery is rarely “how big is the tank” and more often “how much of the vintage’s volume range does this one vessel actually need to cover.”
When Variable Capacity Actually Matters
The common assumption is that any winery bottling multiple small lots should default to variable-capacity tanks across the board. That’s not always the cheaper or more practical call.
Variable capacity earns its premium when a lot sits in the same vessel through several partial-volume stages — primary fermentation, then racking off lees, then topping during aging, then blending trials — without being moved to a smaller tank at each step. If a winery instead presses to barrel or moves to a bottling tank shortly after fermentation finishes, a fixed tank sized close to the batch volume does the same job for less money.
One limitation worth flagging before ordering: most floating-lid designs only adjust within a defined range of the tank’s total height, generally somewhere in the range of a fifth to a third of nominal volume, not the full 0–100% span. A tank rated for 5,000L variable capacity is not necessarily usable down to a few hundred liters — that detail lives in the manufacturer’s mechanical drawing, not the marketing copy, so it has to be confirmed per model rather than assumed.

Sizing Tradeoffs for Wineries Producing Multiple Varietals
A winery running four or five small varietal lots at once is really solving an inventory problem, not just a tank-capacity problem. Two sizing approaches show up in practice:
- One tank per lot, sized to the largest expected volume for that varietal— simple to manage, but tanks sit under-filled for most of the season if yields vary year to year.
- Fewer, larger variable-capacity tanks shared across lots at different stages— reduces total vessel count, but requires more careful scheduling since two lots can’t occupy the same tank simultaneously.
The second approach is where variable capacity pays for itself fastest: a single tank can hold a 3,000L Cabernet lot through fermentation, drop with it through racking, then be cleaned and refilled with a 4,500L Chardonnay lot from the next block — all within one vessel’s adjustment range, rather than owning two separate fixed tanks sized for each lot’s peak volume.
MICET’s Documented Wine Tank Specifications — and Where the Catalog Falls Short of This Format
MICET’s published wine fermentation tank line lists two reference capacity points: 5,000L and 10,000L, built in SUS304 or SUS316L stainless steel, with an inner shell around 3.0mm and outer shell around 2.0mm, insulated with 80–100mm of polyurethane.
| Documented Spec | Value |
| Reference capacities | 5,000L / 10,000L (example sizes cited) |
| Shell material | SUS304 or SUS316L |
| Inner shell thickness | ~3.0mm |
| Outer shell thickness | ~2.0mm |
| Insulation | 80–100mm polyurethane |
| Certification (product-line level) | Not disclosed for wine tanks specifically |
Here is the gap that matters for this topic: MICET’s public wine tank line does not itemize a floating-lid or telescoping variable-capacity configuration. The two capacity points on file are fixed-volume reference examples. If a floating-lid version is available, it would fall under custom engineering rather than a standard catalog SKU — and that has to be confirmed directly with MICET’s sales team before assuming it’s an off-the-shelf option. Wineries evaluating this format against MICET should ask for a mechanical drawing showing the lid’s adjustment range in liters, not just a maximum nominal capacity.
On certification: MICET holds a Verification of Conformity under the Pressure Equipment Directive (PED 2014/68/EU), certificate number ICR/VC/HM2507146, issued by ICR Co., Ltd., valid through July 15, 2030. That verification covers brewing, brewing-adjacent, and fermentation equipment as pressure vessels at an organization/product-line level — it is not itemized against wine tanks by name, and it does not by itself confirm certification status for a specific floating-lid or variable-capacity unit. Ask for the exact scope document if PED coverage for a wine tank purchase is a requirement.
What to Ask Before You Buy
- Request the lid’s actual adjustment range in liters, not just the tank’s maximum nominal capacity — a 5,000L tank might only float down to 3,500L.
- Ask whether the gasket and seal material are wine-contact rated, since some floating-lid designs are adapted from beer or industrial tank lines.
- Confirm whether the configuration is a standard catalog item or custom engineering, since lead time and pricing differ substantially between the two.
- Get pricing in writing for the specific capacity and material grade, since neither format has a published price band for wine tanks in MICET’s public materials — commercial brewery and microbrewery equipment ranges are published, but wine tank pricing is quote-only.
- Ask which certifications, if any, apply to the specific unit being quoted, rather than assuming an organization-level PED verification transfers automatically to that model..
FAQ
Q: Does a variable-capacity wine tank replace the need for a separate small-lot tank?
A: Sometimes. If the lid’s adjustment range covers the full volume swing a lot goes through — from fermentation peak down to final topped volume — one tank can do the work of two fixed vessels. If the swing exceeds the lid’s rated range, a second smaller tank is still needed.
Q: Is variable capacity worth it for a winery producing one or two varietals only?
A: Less often. The cost premium is easiest to justify when the same vessel cycles through multiple volume-reduction stages across several lots in a season. A single-varietal operation moving straight to barrel after fermentation gets less benefit from the format.
Q: Can an existing fixed tank be retrofitted with a floating lid?
A: This depends entirely on the tank’s shell diameter tolerance and whether a matching lid and seal system exists for that diameter — it is a case-by-case mechanical question for the manufacturer, not a standard aftermarket part.
Q: Are MICET’s wine tanks certified under a specific pressure equipment standard?
A: MICET holds an organization-level PED Verification of Conformity (ICR/VC/HM2507146, issued by ICR Co., Ltd., valid to July 2030) covering fermentation and pressure vessel equipment broadly. No wine-tank-specific certificate number is published, so confirm scope for the exact unit being quoted.
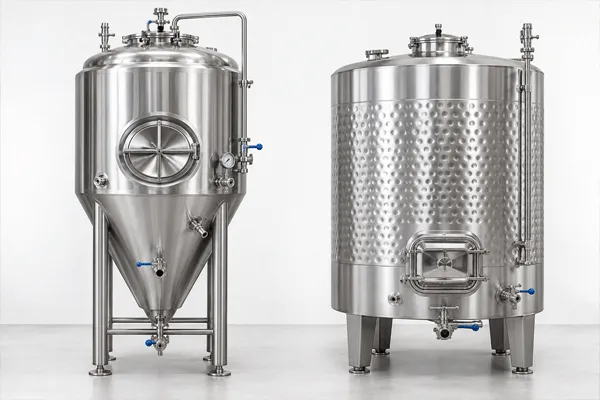
Used Stainless Steel Tanks for Sale: Beer, Wine, Beverage
Nancy Shang | Founder & CEO, MICET | Published September 10, 2026
Used equipment listings, asking prices, and available inventory change weekly. The verification steps below stay valid regardless of market conditions, but always confirm current availability and documentation directly with the seller before purchase.
Why “Used” Means Different Things Across Beer, Wine, and Beverage
A tank that worked perfectly in a winery for a decade is not automatically ready for a brewery, and the reverse is just as often false. The three industries share a base material — 304 or 316 stainless steel — but the tank geometry, internal fittings, and thermal setup diverge in ways that matter once you’re the one signing the purchase order.
Beer fermenters are usually cylindroconical, with a 60-70 degree cone bottom for yeast harvesting and a glycol jacket wrapped around the cylinder for temperature control during active fermentation. Wine tanks more often run flat or dish-bottomed, since winemakers rack off sediment rather than harvest yeast, and many operate without any jacket at all — ambient cellar temperature does the work instead. General beverage process tanks (juice, kombucha, RTD cocktails) split the difference: some carry jackets for pasteurization or cold-crashing, others are simple holding vessels with no temperature control hardware.
Buy a used wine tank thinking it will drop into a beer fermentation line, and you’ll likely be retrofitting a jacket, adding a cone, or accepting a flat-bottom compromise that makes yeast management harder. This is the single most common cross-category mistake integrators and distributors run into when sourcing on price alone.
Tank Types and the Applications They Actually Fit
| Tank Type | Typical Material | Primary Use | Key Fit-for-Purpose Feature | Cross-Category Reuse |
| Cylindroconical Fermenter | SUS304, glycol jacket | Beer, some kombucha | Cone bottom for yeast/trub drop | Poor fit for wine; possible for kombucha with cleaning |
| Bright/Brite Tank | 304/316, pressure-rated | Beer carbonation & storage | Pressure-reducing valve, CIP nozzle | Rarely reused outside beer without re-certification |
| Variable Capacity Wine Tank | 304/316, floating lid or fixed | Wine, cider | Adjustable headspace, minimal oxygen exposure | Adaptable to beverage holding with lid modification |
| Flat-Bottom Process Tank | 304, jacket optional | Kombucha, juice, mixing | Simple geometry, wide manway | Most versatile across categories |
| Horizontal Storage Tank | 304, insulated variants | Beverage staging, bulk holding | Space-efficient footprint | Works across all three if internals are food-grade |
The flat-bottom process tank column explains why so many used-tank marketplaces are dominated by general mixing vessels rather than fermenters: they’re the easiest to repurpose, so sellers move them fastest and buyers across categories compete for the same inventory.
How to Verify a Used Tank Before You Buy
Photos and a seller’s word are not verification. Here’s the sequence that actually protects a purchase.
- Request the mill certificate for the shell material. A mill cert confirms whether the tank is genuinely 304 or 316 stainless — visual inspection cannot tell the difference, and mislabeled 201-grade substitutes do circulate in secondary markets, particularly on tanks sourced through resellers rather than original fabricators.
- Ask for the tank’s pressure history if it ever ran carbonated or pressurized product. Brite tanks and some fermenters operate under internal pressure, which is why new pressure vessels in this category typically carry documentation against a directive such as the EU’s 2014/68/EU Pressure Equipment Directive. If a used pressure-rated tank has no test or verification record at all, budget for a fresh inspection before it goes back into service.
- Inspect welds and the interior surface for pitting, especially near the CIP spray ball and any sanitary fittings. Pitting corrodes food-grade finish integrity and creates harborage points for bacteria that ordinary cleaning cycles won’t reach.
- Pressure- or vacuum-test the glycol jacket separately from the vessel itself, if the tank has one. Jacket leaks are common on tanks that sat idle for years, and a slow leak won’t show up until the tank is already running a batch.
- Match every manway, tri-clamp, and fitting size against your existing piping before purchase, not after delivery. This is the edge case buyers underestimate most: a tank can be structurally perfect and still cost you weeks of custom fabrication because the outlet is 2-inch tri-clamp and your line runs 3-inch.
- Confirm the tank’s prior contents, including anything non-beverage. Stainless steel resists many chemicals, but a tank that held solvents, dairy with high fat residue, or industrial process fluid needs documented cleaning and, in some jurisdictions, re-certification for food contact before it touches a beverage product. “It’s stainless, so it’s food-safe” is the misconception that causes the most expensive mistakes in this market — the metal being food-grade doesn’t mean the tank’s history is.What Certification Standards Tell You About a Used Tank’s Reliability
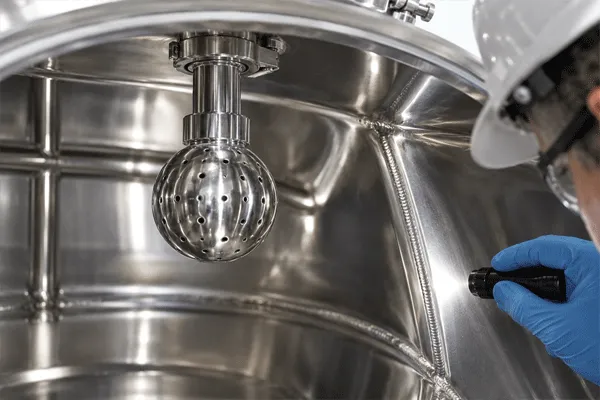
New pressure-rated equipment in this category is typically sold against a documented compliance trail — for example, MICET’s own tanks carry PED Verification 3N231110.SICS093, issued by Ente Certificazione Macchine Srl and valid through November 2028, tested against EN 1626:2008. That document specifies the exact standard, the issuing body, and an expiration date, which is what separates third-party verification from a manufacturer’s own self-declaration.
When you’re evaluating a used tank, that same standard of documentation is the benchmark to ask for, even informally. A seller who can produce a dated inspection report from a named testing body is offering something categorically different from a seller who says “it passed everything when we used it.” If no such record exists, treat the tank as unverified and price your offer, or your post-purchase inspection budget, accordingly.
New vs. Used: What Actually Changes
| Factor | New Tank | Used Tank |
| Upfront cost | Higher, fixed | Lower, negotiable |
| Certification documentation | Included from manufacturer | Depends entirely on seller records |
| Warranty | Standard manufacturer warranty | Rarely, unless explicitly negotiated |
| Lead time | Weeks to months for fabrication | Often available immediately |
| Customization | Built to your spec (jacket, ports, capacity) | Fixed as-is, retrofits add cost |
| Total cost of ownership | Predictable | Variable, depends on inspection findings |
The lead time column is where used tanks win outright for buyers facing a capacity crunch this quarter rather than next year. The certification column is where new tanks win outright for buyers who need audit-ready documentation for a commercial contract or a lender.
Pricing Reality for Buyers
Used tank pricing varies by seller, condition, and region enough that no reliable general figure exists, and any number quoted without a specific tank in front of you should be treated as a rough placeholder, not a quote. What can be stated with certainty is new-equipment pricing where it has been published: MICET’s microbrewery-scale systems run 30,000-80,000 USD, and commercial systems starting at the smallest 10bbl configuration run 50,000-80,000 USD. Everything outside those two published bands, new or used, requires a direct quotation against your specific specs.
If a used listing looks significantly below what a comparable new system would cost, that gap is worth investigating rather than celebrating. Ask what’s driving the discount: age, missing documentation, non-standard fittings, or genuine seller motivation to move inventory quickly. All four are legitimate reasons a used tank is cheap, but they carry very different risk profiles.
When New Makes More Sense Than Sourcing Used
For buyers evaluating a used fermentation tank specifically, the calculation usually comes down to how much documentation gap you’re willing to absorb. A used fermenter with no material certificate, no pressure history, and unknown prior contents isn’t necessarily a bad tank, but it is an unverified one, and verifying it after the fact (independent lab testing, re-inspection, potential jacket repair) can close much of the price gap that made it attractive in the first place.
MICET’s core business is building new brewing, fermentation, and process tanks to order rather than brokering used inventory, so our role here is sharing what our own certification and fabrication process looks like as a reference point for what “verified” should mean, not steering every reader toward a new purchase regardless of budget. For a buyer with a tight timeline and a tank in hand that checks out against the six-point list above, used remains a sound decision. For a buyer who needs bank-ready documentation, product traceability for export markets, or a jacket and cone configuration that doesn’t exist in the used market near them, a new build closes that gap without the inspection uncertainty.
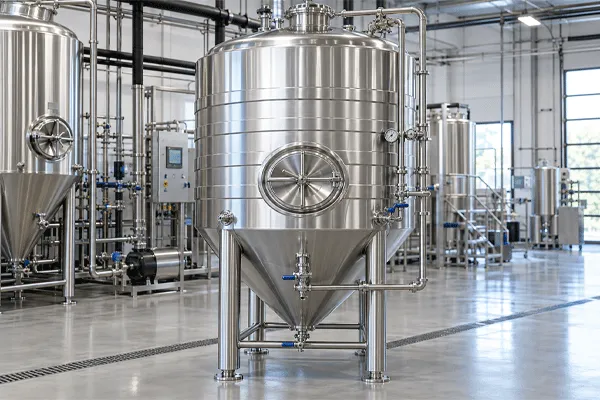
How This Compares to Typical Used-Equipment Listings
Most secondary-market listing platforms for stainless tanks provide a photo set, an asking price, and a brief condition description written by the seller rather than an independent inspector. That’s workable for buyers who plan to inspect in person before paying, but it puts the verification burden entirely on the buyer’s side of the transaction — there’s no standardized documentation requirement the way there is for new pressure equipment sold against a directive like PED. Treat any listing platform’s condition notes as a starting point for your own six-step check, not a substitute for it.
FAQ
Q: Can a used wine tank be converted into a beer fermenter?
A: Sometimes, but expect retrofit costs. A flat-bottom wine tank can hold beer, but without a cone bottom, yeast harvesting becomes manual and less efficient, and adding a glycol jacket after the fact is a fabrication job, not a bolt-on accessory.
Q: Is 304 stainless enough, or do I need 316 for beverage tanks?
A: 304 handles most beer, wine, and standard beverage production without issue. 316 adds molybdenum for better resistance to chloride and acidic environments, which matters more for certain wine styles, high-acid kombucha, or coastal locations with saline air exposure during storage.
Q: How do I check PED compliance on a used pressure vessel?
A: Ask the seller for the original test or verification report, including the issuing body’s name and the standard tested against (EN 1626:2008 is common for this category). No report means no verified compliance, regardless of what the seller states verbally.
Q: What’s a fair price for a used commercial fermentation tank?
A: There’s no reliable general figure — condition, documentation, capacity, and region all move the number too much. Use published new-equipment pricing as a ceiling reference and negotiate the used price down from there based on your inspection findings.
Q: Does MICET sell used tanks, or only new?
A: MICET fabricates new tanks built to customer specifications. This guide shares our verification and certification standards as a reference for evaluating used equipment, not as a used-inventory listing.
Q: What paperwork should come with a legitimate used tank sale?
A: At minimum, a material mill certificate. For any pressure-rated vessel, a pressure test or verification record with a named issuing body and date. For food-contact use, documentation of prior contents and cleaning history.
If your inspection turns up a documentation gap you can’t close, or a fitting mismatch that would cost more to retrofit than the tank saved you, a new build quoted against your exact capacity and jacket requirements is worth comparing before you commit to the used option.
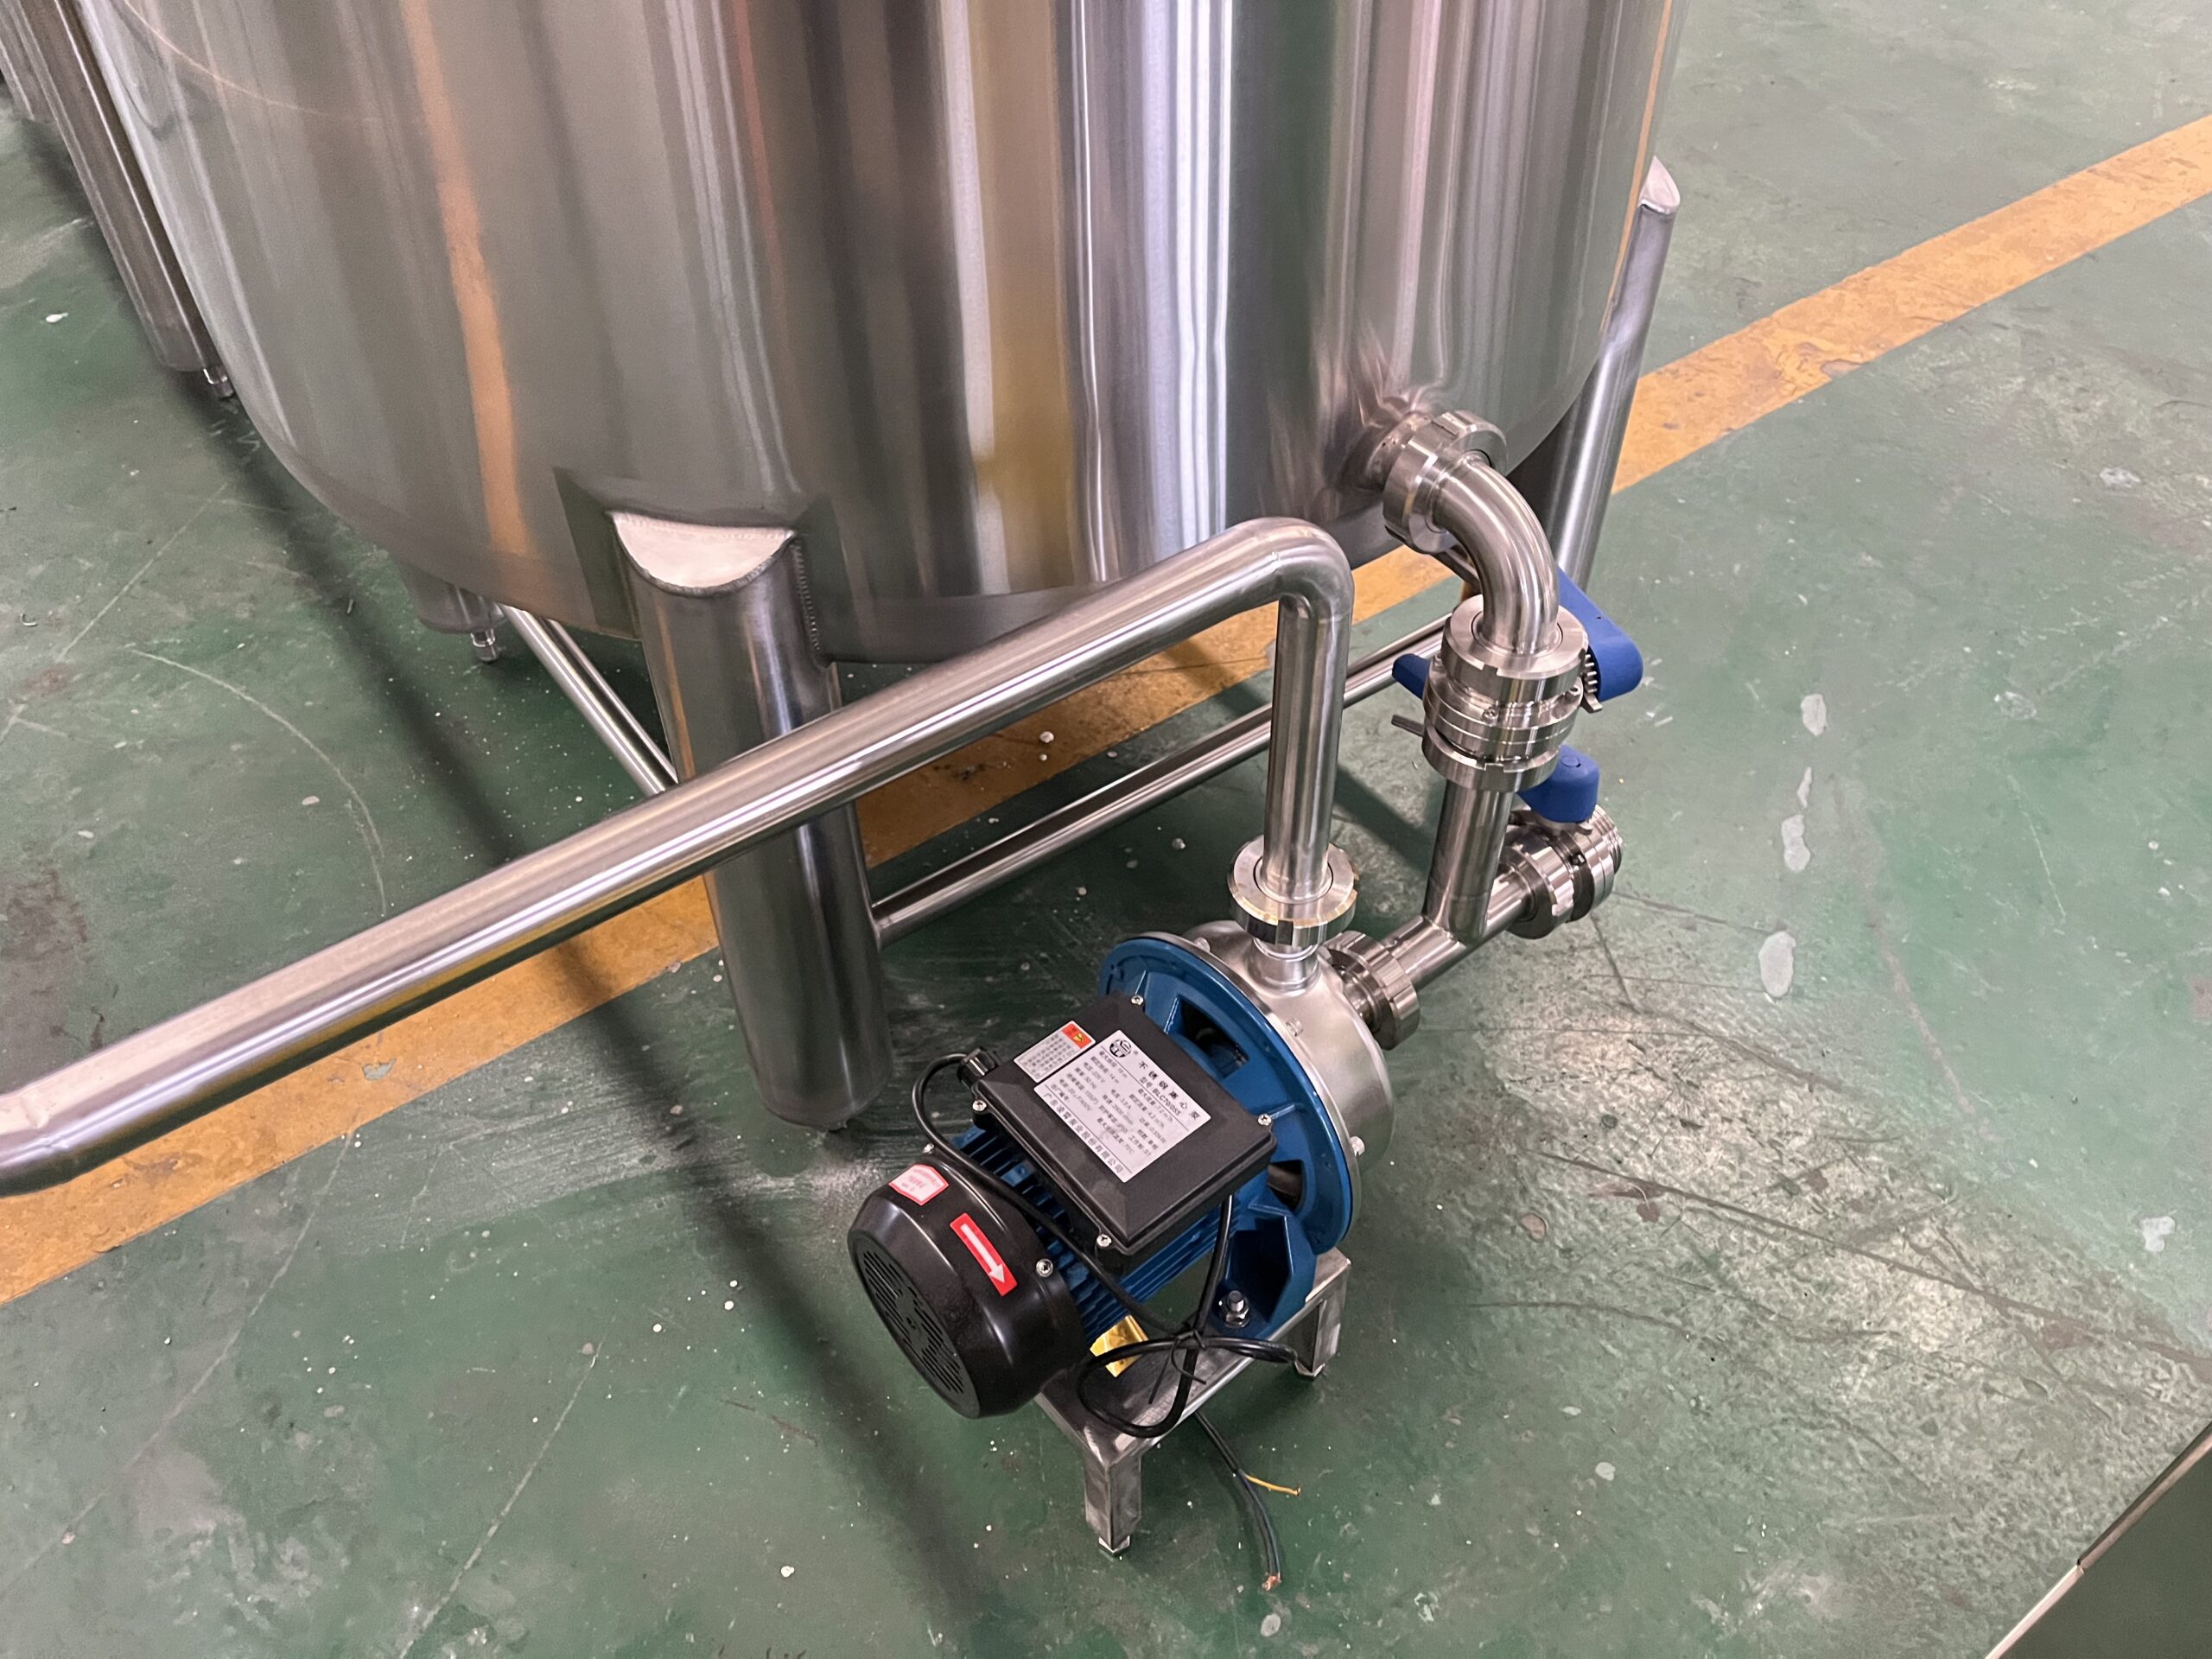
Brewery Pumps: Types and When to Replace vs Refurbish
Nancy Shang | Founder and CEO, MICET Brewing | Published September 9, 2026
Most brewhouses run on two pump types: centrifugal pumps for wort and water transfer, and positive-displacement pumps for thick or particulate-heavy liquids like mash or trub slurry. Deciding whether to refurbish or replace one comes down to three checkpoints — service hours, seal condition, and impeller wear — not just whether it still turns on.
What Are the Two Main Brewery Pump Types?
Centrifugal pumps move liquid using a spinning impeller that flings fluid outward through a volute casing. They handle thin, low-viscosity liquids well — wort transfer, whirlpool recirculation, CIP fluid movement — but performance drops sharply if the liquid gets thick or contains solids that can clog the impeller vanes.
Positive-displacement (PD) pumps — lobe, diaphragm, or progressive-cavity designs are the common brewery variants — move a fixed volume of fluid per rotation regardless of viscosity. That makes them the right choice for mash transfer, hop slurry, yeast slurry, or any liquid with suspended solids where a centrifugal pump would lose flow or clog.
A brewery running a standard brewhouse package typically needs both: centrifugal for the clear-liquid transfers, PD for anything with body or particulates.
Where Each Pump Type Is Used in a Brewhouse
| Task | Typical Pump Type | Why |
| Wort transfer (kettle to whirlpool/HLT) | Centrifugal | Low viscosity, high flow rate needed |
| CIP fluid circulation | Centrifugal | Clean liquid, consistent flow |
| Mash transfer | Positive-displacement | Viscous, contains grain solids |
| Trub/hop slurry removal | Positive-displacement | Particulate-heavy |
| Yeast slurry handling | Positive-displacement | Shear-sensitive, needs gentle constant-volume movement |
How to Decide: Replace vs Refurbish
This applies whether the pump came with a new brewhouse package or arrived as part of a used equipment purchase with an unknown history.
- Check documented service hours, if available.A pump with a logged maintenance history and moderate run time is a stronger refurb candidate than one with no records at all.
- Inspect the mechanical seal.Look for visible leakage at the shaft, scoring on the seal face, or a burnt smell from dry-running. A worn seal alone is usually a refurb-level fix — it does not automatically mean the pump needs replacing.
- Inspect the impeller for wear or pitting.Cavitation damage (pitted, eroded impeller vanes) reduces flow and head pressure permanently. Light wear can sometimes be tolerated; heavy pitting is a sign the pump is losing efficiency it won’t get back without a new impeller.
- Check the shaft and bearings for play.Wobble or noise under load points to bearing wear, which is repairable but adds labor cost on top of parts.
- Weigh refurb parts and labor against replacement cost.If the motor, casing, and shaft are sound and only the seal or impeller needs work, refurbishing is usually the lower-cost path. If the casing shows corrosion damage or the motor has failed, replacement is typically the more defensible call — get quotes for both before deciding, since exact costs depend on pump size, brand, and local labor rates.
- Confirm food/beverage-contact material compatibility before refurbishing.A replacement seal or impeller in the wrong material (wrong elastomer, wrong wetted-part alloy) can introduce a contamination or corrosion risk even if it fits mechanically.
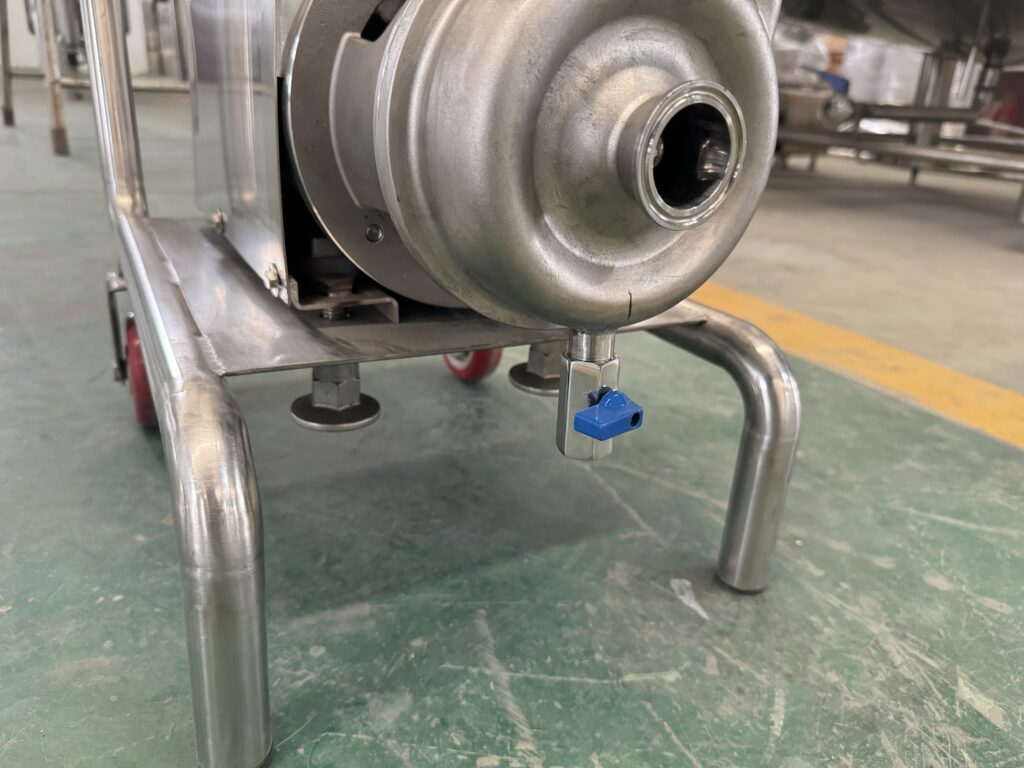
The Misconception Worth Correcting
“It still runs, so it’s fine” is the most common mistake in this decision. A pump can run for years past the point where its impeller has lost enough material to reduce flow rate and head pressure below what the process actually needs — the pump doesn’t fail outright, it just quietly underperforms, and the brewer compensates by running longer cycles without realizing the pump is the bottleneck. Checking flow rate against the pump’s original rated curve, not just whether it turns on, is the more reliable test.
The Edge Case: Used Equipment With No Service History
A pump bought as part of a used brewhouse package rarely comes with a maintenance log. In that case, step 1 above (checking documented service hours) isn’t usable, and the decision has to rest entirely on physical inspection — seal condition, impeller wear, bearing play, and a flow-rate test against the process requirement, not assumed remaining life based on age or brand reputation.
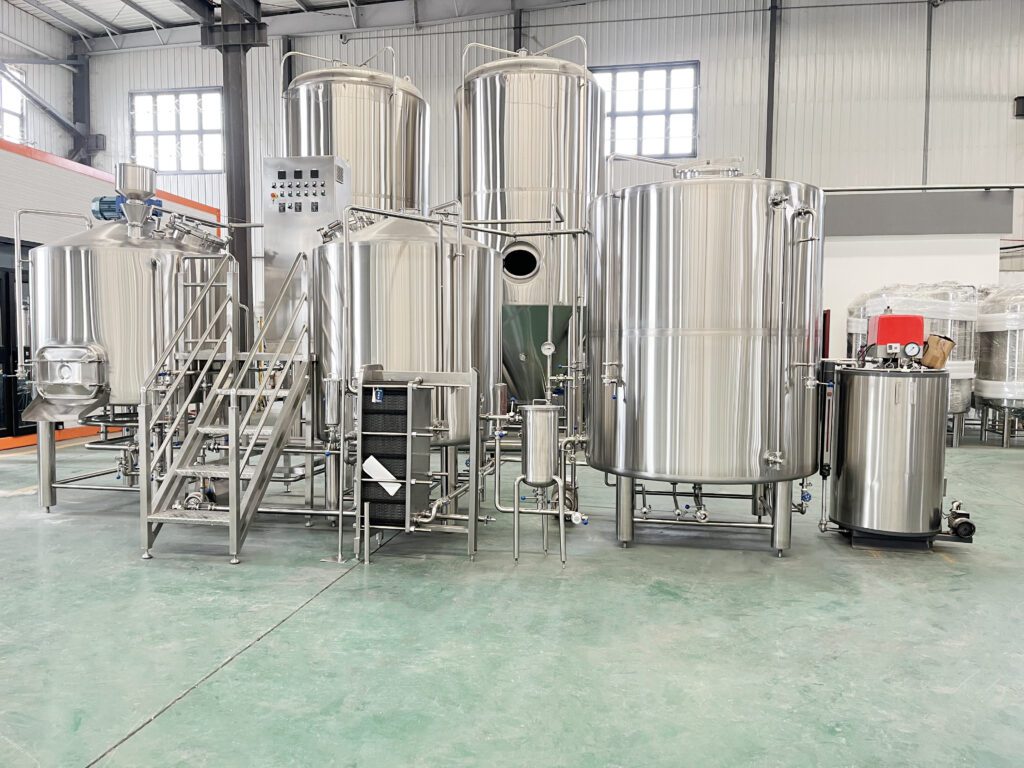
What MICET’s Used Brewery Equipment Line Discloses on Pumps
MICET’s used brewery equipment listings describe 2–10 bbl compact brewhouse configurations that include a mash tun, kettle, and HLT package, with pumps, a heat exchanger, and a control panel included in the package. What the published catalog does not itemize is pump-specific data — flow rate, horsepower, wetted-part material, or seal type for the pumps bundled into a given used package. A buyer evaluating a specific used brewhouse should request that data directly rather than assuming a standard spec across all listed units, since “pumps included” describes package composition, not a fixed pump model.
On certification: MICET’s used brewery equipment line references general “ASME/CE” craftsmanship without a specific certificate number or issuing body attached to that line. Separately, MICET holds a PED Verification of Conformity — certificate 3N231110.SICS093, issued by Ente Certificazione Macchine Srl, covering brewing, beer, and brewery equipment as pressure vessels, valid through November 9, 2028. That verification sits at the organization/product-line level for MICET’s equipment broadly; it does not certify any individual used or refurbished unit, and it should not be read as covering a specific secondhand pump’s condition or compliance status. Ask for unit-specific documentation, not the organization-level certificate, when compliance matters for a used purchase.
FAQ
Q: Can a centrifugal pump be used for mash transfer if that’s all I have on hand?
A: It will move liquid, but expect reduced flow and more frequent clogging on anything with grain solids. It’s a workaround, not a long-term substitute for a positive-displacement pump in that role.
Q: How often should mechanical seals be inspected?
A: There’s no single interval that fits every brewery — it depends on run hours and the liquid being pumped. Visual inspection at each CIP cycle and a closer check at scheduled maintenance intervals catches most seal issues before they cause downtime.
Q: Does a used pump with no paperwork automatically mean skip it?
A: Not automatically. Missing service history means the decision rests on physical inspection instead of records — a pump that passes seal, impeller, and flow-rate checks can still be a reasonable refurb candidate even without a maintenance log.
Q: Is MICET’s organization-level PED certificate enough documentation for a used pump purchase?
A: No — that certificate applies at the organization/product-line level to MICET’s equipment broadly and doesn’t certify a specific used or refurbished unit. Request unit-specific documentation separately if certification matters for the purchase.